
Boiler manufacturing combines heavy plate processing, high-integrity pressure-part welding, and strict code compliance into one connected workflow. A complete production line solution must coordinate CNC cutting, panel forming, membrane panel welding, tube bending, fin-bar calibration, and final header and shell welding so each station feeds the next without unnecessary handling or rework. The result should be measured not only in output per shift, but in dimensional stability, repeatable weld quality, and a documented fabrication chain that can withstand third-party inspection.
Need a line configuration and budget estimate for your boiler panel capacity? Send panel width, tube diameter, and target shift output to jay@weldc.com or call +86-13815101750.

What a Complete Boiler Production Line Covers
A complete boiler manufacturing line typically includes plate storage and edge preparation; CNC plasma, laser, or flame cutting; tube cutting and end preparation; membrane panel welding; panel bending; fin-bar calibration for economizer panels; tube-to-tube and header-to-tube welding; rotation, lifting, and positioning equipment; welding manipulators; and nondestructive examination stations. ASME Boiler and Pressure Vessel Code Section I [1] sets construction rules for power boilers, while EN 12952 [2] regulates water-tube boilers and auxiliary installations for the European market. ISO 3834 [3] adds a quality management framework for fusion welding, including welding coordination, procedure qualification, and inspection records. A line designed around these requirements embeds material traceability, weld maps, and inspection gates into the material flow instead of adding them after fabrication.
Equipment Blocks in a Boiler Panel Line
Cutting and Edge Preparation
Boiler plate and tube materials require square, consistent cut edges before welding. CNC plasma and laser cutting cells can process alloy steel plate with the edge quality needed for panel assembly. A CNC plasma cutter or CNC laser cutting machine should be selected by plate thickness, required bevel geometry, and cutting table utilization. Cutting accuracy directly affects panel fit-up, because a plate edge that varies beyond tolerance creates the same variation in the first membrane weld pass.
Membrane Panel Welding
Membrane panel welding is the heart of boiler furnace wall and economizer production. The process joins tubes to membrane bars with controlled penetration and minimum distortion. A dedicated membrane panel welding machine keeps tube spacing and bar alignment stable during welding, which is essential for code-compliant panel width and straightness. In high-volume serial production, the machine must support quick changeover between different tube diameters and panel widths without losing weld parameter repeatability.
Panel Bending and Forming
Some boiler panels require bending to match furnace shape or assembly access. A panel bending machine performs the necessary bending after welding or as a pre-forming operation, depending on product design. Tooling condition and bend sequencing are as important as machine tonnage, because springback and edge marking can create downstream fit-up problems.
Tube Booster Bending and Header Preparation
Header fabrication requires tube bending for close-pitch tube arrangements and return bends. A tube booster bending machine provides the controlled boost and die support needed for small-radius bends without wrinkles or excessive ovality. Bending should be planned together with tube end preparation so that every bent tube arrives at the header fit-up station with the correct orientation and stickout.
Fin-Bar Calibration
For economizer and heat-recovery panels, fin-bar geometry directly influences heat transfer and weld consistency. A fin bar calibration machine corrects bar shape, straightness, and spacing before welding. Calibration after shearing and before panel welding reduces the chance of gaps, misaligned bars, and local heat-transfer variation.
Tube-to-Tube and Header Welding
Tube-to-tube and tube-to-header welding demand full-penetration joints with tight fit-up. A tube-to-tube welding machine can standardize torch angle, oscillation, and travel speed for repetitive joints, while rotating the workpiece instead of forcing the welder to change position. For larger headers and drums, a welding manipulator keeps the welding head on the seam centerline while positioners and rotators turn the component.
Rotating, Lifting, and Positioning
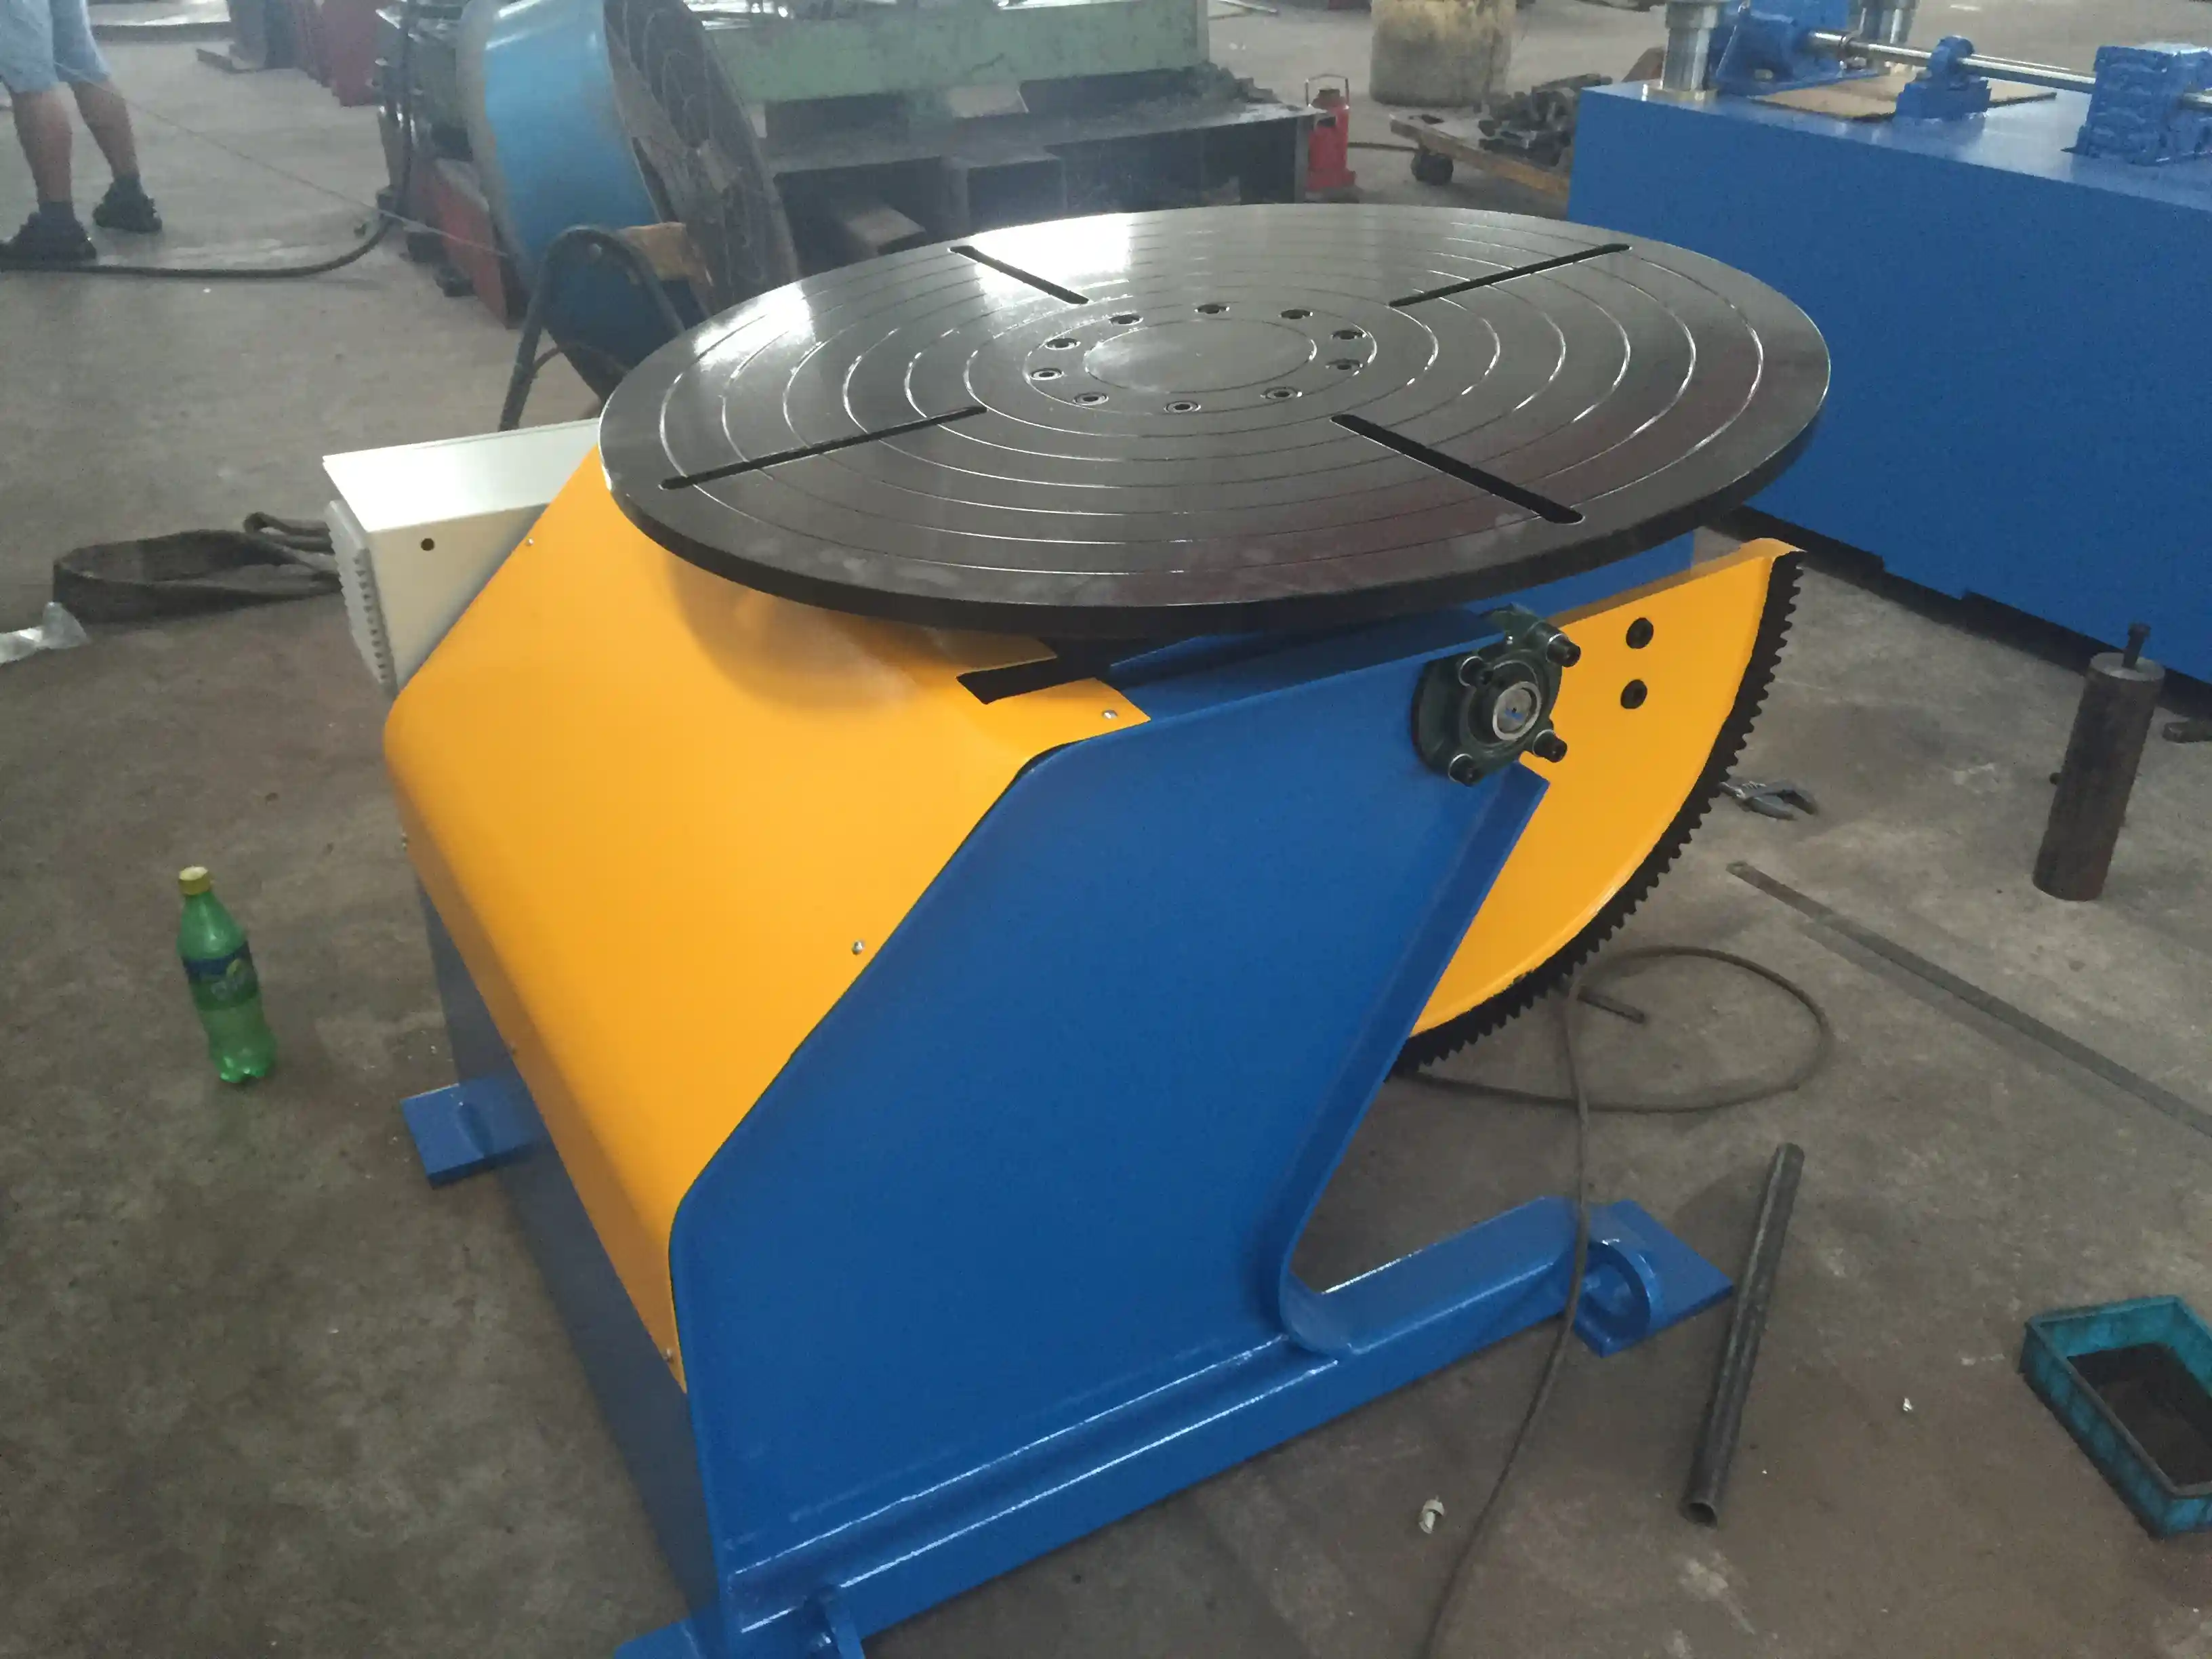
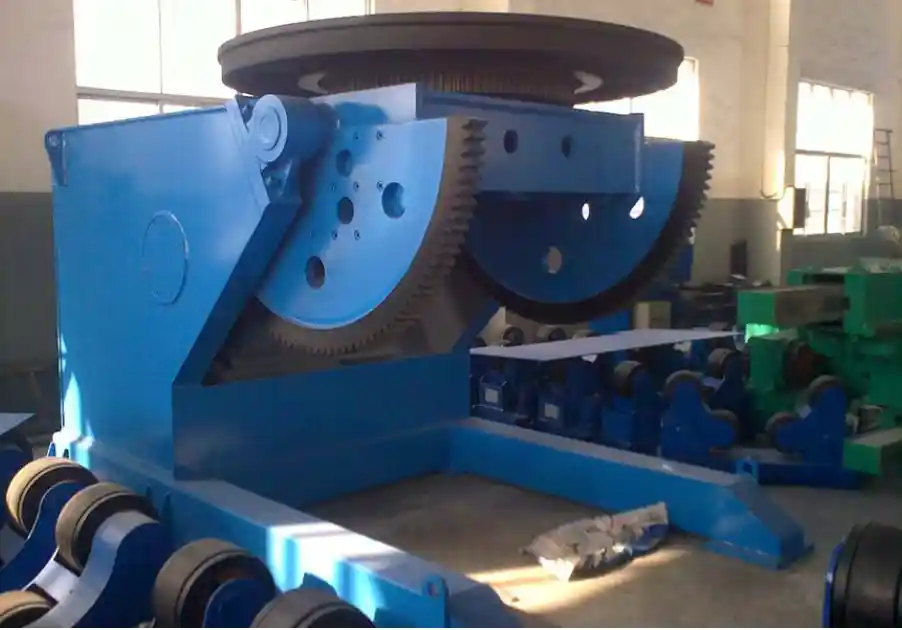
Heavy boiler drums, headers, and panel assemblies require precise rotation and tilt to keep welding in the correct position. A 3-axis precision positioner provides synchronized turning, continuous rotation, and tilting for smaller pressure components, with product documentation listing ±0.05 mm positioning accuracy and 0.02 mm repeatability. The same positioning logic applies to larger vessels, where controlled rotation prevents weld mismatch and reduces the need for repair.
Rotating heavy boiler drums and headers without precise speed control creates uneven heat input and weld defects. <Improving Quality and Efficiency in Tank and Pressure Vessel Manufacturing: The Core Application Value of Positioners> covers how controlled rotation and positioning improve fit-up and pass rates in pressure-part fabrication.
Boiler drums and header shells are pressure vessels with similar fit-up and weld requirements. <Wuxi ABK Professional Welding Rotary Equipment: Precision Welding Solution for Pressure Vessel Manufacturing> examines rotary equipment selection for longitudinal and circumferential seam welding on pressure-retaining components.
Large-diameter boiler headers and downcomers need consistent rotation for full-penetration groove welds. <Achieving Perfect Welds on Large-Diameter Pipes with Professional Rolling Equipment> covers rolling-equipment setup and welding parameters that reduce misalignment and improve seam quality.

Quality and Code Compliance
Welding Qualification and Documentation
Pressure-retaining welds require a qualified welding procedure specification and documented procedure qualification records. ASME BPVC Section IX [4] governs welding, brazing, and fusing qualifications when the boiler is built to ASME rules. A production line should therefore include equipment that supports repeatable parameters, such as PLC-stored programs and controlled travel speed, because a qualified WPS has limited practical value if the production equipment cannot execute it consistently.
Nondestructive Examination and Inspection Gates
ASME BPVC Section V [5] provides methods and requirements for nondestructive examination. A complete boiler line usually places inspection gates after membrane panel welding, after header fit-up, and after final pressure-part welding. The specific combination of visual examination, penetrant, magnetic particle, ultrasonic, or radiographic testing depends on joint category, material, and contract requirements. In-line inspection prevents a defect from moving downstream to assembly, where repair is more expensive and more difficult.
Line Configurations by Panel Width, Tube Size, and Output
| Line block | Key equipment | Main selection variables |
|---|---|---|
| Plate and tube cutting | CNC plasma/laser/flame cutter | Material thickness, bevel type, table length |
| Membrane panel formation | Membrane panel welding machine | Panel width, tube diameter, bar thickness |
| Panel forming | Panel bending machine | Bending force, maximum length, tooling |
| Header and tube welding | Tube-to-tube welding machine | Tube outside diameter, joint type, torch count |
| Rotating and positioning | Welding manipulator, rotator, positioner | Load capacity, vessel diameter, speed range |
Small-Batch Job Shop vs Serial Boiler Panel Production
For a low-volume high-mix job shop, modular equipment and quick-change fixtures reduce setup time between different panel widths and tube pitches. For serial boiler panel production, the line should be balanced so that membrane panel welding does not outrun calibration or inspection. The number of parallel welding stations is derived from target output per shift, station cycle time, first-pass yield, and planned maintenance downtime.
Automation and Data Integration
Modern boiler production equipment should be selected for integration, not just standalone performance. PLC and HMI controls make it easier to store welding programs, enforce operator access, and collect parameter records. Robotic interfaces are relevant when a line includes automated welding cells; for example, WUXI ABK 3-axis positioners support ABB, KUKA, FANUC, and Yaskawa interfaces. Seam tracking and arc-voltage control can maintain welding consistency on long membrane seams and circumferential header joints. ISO 3834 [3] requires documented control of welding-related activities, so equipment that records current, voltage, travel speed, and operator identification simplifies compliance.
ROI and Break-Even Considerations
A boiler production line investment should be evaluated on total cost of ownership rather than individual machine price. The main savings come from lower direct labor per ton, higher first-pass yield, less rework, fewer rejected panels, better material utilization from precise cutting and nesting, and improved shop safety. To estimate break-even, compare annual labor and rework savings plus additional capacity value against installed cost and commissioning time. Because product mix and labor rates vary by region, the most reliable analysis uses hours per panel before and after automation, not a generic payback claim.
Common Bottlenecks and How Line Design Solves Them
- Membrane welding mismatch: Controlled fixture spacing, bar alignment, and stitch sequence prevent panel width error from accumulating.
- Fin-bar calibration drift: In-process calibration before welding reduces gaps and thermal-contact variation.
- Tube-to-tube misalignment: Self-centering chucks, rotators, and positioners hold joint alignment while the weld is made.
- Cutting bottleneck: High-productivity CNC cutting with multi-torch or laser options keeps plate and tube supply ahead of welding.
- Inspection backlog: Placing NDT after known critical operations avoids inspecting everything at the end and discovering systemic defects too late.
Get a Complete Boiler Production Line Quote
WUXI ABK MACHINERY CO., LTD supplies boiler production line equipment including membrane panel welding machines, panel bending systems, tube booster benders, tube-to-tube welding machines, CNC cutting systems, welding manipulators, positioners, and rotators. To receive a line configuration and quotation, provide the following information:
- Panel width, tube diameter, tube thickness, and bar thickness
- Target output per shift and annual capacity
- Applicable code requirements: ASME BPVC, EN 12952, ISO 3834, or customer specification
- Available workshop area and material flow direction
- Existing equipment to integrate, if any
Contact Zhang Jian at jay@weldc.com or call +86-13815101750. For office inquiries, call +86-510-83555592 or fax +86-510-83559158.
Frequently Asked Questions
What is the minimum equipment set for boiler membrane panel production?
The core set includes cutting and edge preparation, membrane panel welding, panel bending as required, tube bending and end preparation, and tube-to-tube welding with positioning equipment. Nondestructive examination equipment may be added based on code and contract requirements.
Which standard applies to boiler pressure part welding?
ASME BPVC Section I and Section IX are commonly used for power boilers in ASME jurisdictions, while EN 12952 and ISO 3834 are frequently applied in European and quality-system-driven projects. The contract and jurisdiction determine the governing code.
Can WUXI ABK integrate a line with existing CNC cutting and welding equipment?
Integration is possible when existing equipment has compatible control interfaces and sufficient capacity. WUXI ABK evaluates interface, layout, safety, and data requirements before proposing a line arrangement.
What information is needed for a complete boiler production line quotation?
A complete quotation requires panel dimensions, tube size, bar thickness, target output per shift, code requirements, available space, and existing equipment. These variables determine line layout, station count, and equipment sizing.
How is production capacity calculated for a boiler panel line?
Capacity is calculated from available hours per shift, station cycle time, first-pass yield, changeover time, and maintenance downtime. A balanced line uses these inputs to size the number of parallel membrane welding, bending, and welding stations.
References
[1] ASME Boiler and Pressure Vessel Code, Section I, Rules for Construction of Power Boilers, American Society of Mechanical Engineers.
[2] EN 12952, Water-tube boilers and auxiliary installations, European Committee for Standardization.
[3] ISO 3834, Quality requirements for fusion welding of metallic materials, International Organization for Standardization.
[4] ASME Boiler and Pressure Vessel Code, Section IX, Welding, Brazing, and Fusing Qualifications, American Society of Mechanical Engineers.
[5] ASME Boiler and Pressure Vessel Code, Section V, Nondestructive Examination, American Society of Mechanical Engineers.
If you’re interested, check out these related articles:
Revolutionary Solution for Pressure Vessel Welding: Technical Analysis of 360-Degree Rotating Welding Positioners
Achieving Perfect Welds on Large-Diameter Pipes with Professional Rolling Equipment
Core Pain Points and High-Precision Solutions of Welding Positioners in the Wind Power and Shipbuilding Industries: Comprehensive Technical Analysis
Welding Manipulators for Wind Tower Fabrication: Revolutionizing Production Efficiency
Pipe Rotators and Turning Rolls: Essential Equipment for Modern Pipeline Fabrication
 English
 Español
 Français
 Deutsch
 Português
 Русский