
Water jet cutting has two practical process branches: pure water jet cutting and abrasive water jet cutting. Pure water jet cutting accelerates filtered water through a small orifice and uses the kinetic energy of the water alone to cut. Abrasive water jet cutting adds a stream of hard particles, usually garnet, so the jet can erode materials that water alone cannot handle [1]. Both methods are cold, non-contact processes. Neither method depends on oxidation or melting, which is why water jet cutting is often selected when heat input is a concern.
From a production engineering perspective, the comparison is not about which method is better in every case. It is about which failure mode is cheaper to manage. A pure-water machine is simpler and cleaner when the material range stays inside the soft-material envelope. An abrasive machine extends the same waterjet platform into steel, stainless steel, and thicker section work, but it adds abrasive metering, mixing-tube wear, and spent-garnet disposal.
How Pure Water Jet Cutting Works
Pure water jet systems pump water at pressures commonly in the 40,000–60,000 psi range through a precision orifice. The resulting high-velocity stream cuts soft materials such as foam, rubber, gaskets, textiles, thin plastics, and some food products. Because no abrasive is present, the kerf is narrow and the process is mechanically simple.
The main advantage is process simplicity. There is no abrasive feed, no abrasive-related nozzle wear, and no spent-garnet waste stream. The main limitation is material range. A stream of water alone does not reliably cut hard metals, most structural composites, or thick sections.
How Abrasive Water Jet Cutting Works
Abrasive water jet cutting routes high-pressure water through a mixing chamber where garnet is drawn into the stream. The accelerated particles cut by micro-erosion [2]. This expands the process to carbon steel, stainless steel, aluminum, titanium, stone, glass, and thick composites.
Industrial systems typically use garnet mesh sizes matched to the material and edge finish, with abrasive flow controlled by a metering system. The trade-off is an additional consumable stream, more aggressive wear on the orifice and mixing tube, and a waste stream that contains both water and spent abrasive.
Key Operating Differences
| Factor | Pure Water Jet Cutting | Abrasive Water Jet Cutting |
|---|---|---|
| Cutting action | High-velocity water erosion | Water-accelerated garnet particle erosion |
| Material range | Foam, rubber, thin plastics, textiles, some food products | Steel, stainless steel, aluminum, composites, stone, glass |
| Typical thickness | Mostly thin soft-material sections | Thin sheet to thick plate, depending on pump power and material |
| Kerf width | Narrow, often under 1 mm | Wider, often 0.5–1.5 mm depending on nozzle and material |
| Edge quality | Smooth on suitable soft materials; may fray fibrous materials | Often smooth and machined-like on hard materials; slight taper possible |
| Consumables | Water treatment and pump maintenance | Garnet abrasive, orifice, mixing tube |
| Waste stream | Water and removed soft material | Water, spent garnet, and removed hard material |
| Operating cost focus | Pump power, filtration, water use | Abrasive consumption, nozzle wear, abrasive disposal |
These differences are not quality grades. They are capability and cost trade-offs. A pure-water cut can be extremely clean on the right material, while an abrasive cut on steel may require secondary cleanup if the nozzle is worn or the traverse rate is pushed too high.
Material Thickness, Kerf, and Edge Quality
Edge quality is influenced by pump pressure, orifice condition, abrasive mesh, traverse speed, standoff, and the material itself. In metal cutting, edge taper is one of the most common process-control issues. The jet tends to produce a slightly wider entry at the top surface, and slower traverse combined with good nozzle condition reduces taper. Surface texture studies show that traverse speed and abrasive flow rate directly affect finish quality [3].

For shop-floor specification, a useful rule is to validate the actual part edge before committing to a speed target. The same waterjet platform can produce very different results on 3 mm stainless steel and 50 mm carbon steel.
Selecting a Method by Material and Production Goals
Pure water jet cutting is usually the stronger choice when the workload is dominated by soft materials, narrow kerf requirements, and simple waste handling. It also works well for high-volume thin gaskets, seals, and foam products.
Abrasive water jet cutting is usually required when the part mix includes metal, glass, stone, or thick composites. For mixed work, an abrasive machine offers a broader platform, but the cost of garnet and pump hours should be modeled before deciding that one machine must handle every job. A dedicated pure-water machine can be lower-cost for high-volume soft-material cutting.
Equipment and Production Line Integration
Both methods can be run on CNC gantry systems with catcher tanks, water treatment, and PC-based controls. The process decision should be made before the table is specified because the nozzle assembly, pump rating, and waste handling differ.
A CNC water jet cutting machine is usually matched to a fixed cutting tank, gantry, and material-handling plan. For thin soft-material field work, a portable water jet cutter can be a lighter and more flexible option. Shops that combine cutting with welding should evaluate how the cut part moves into the next station.

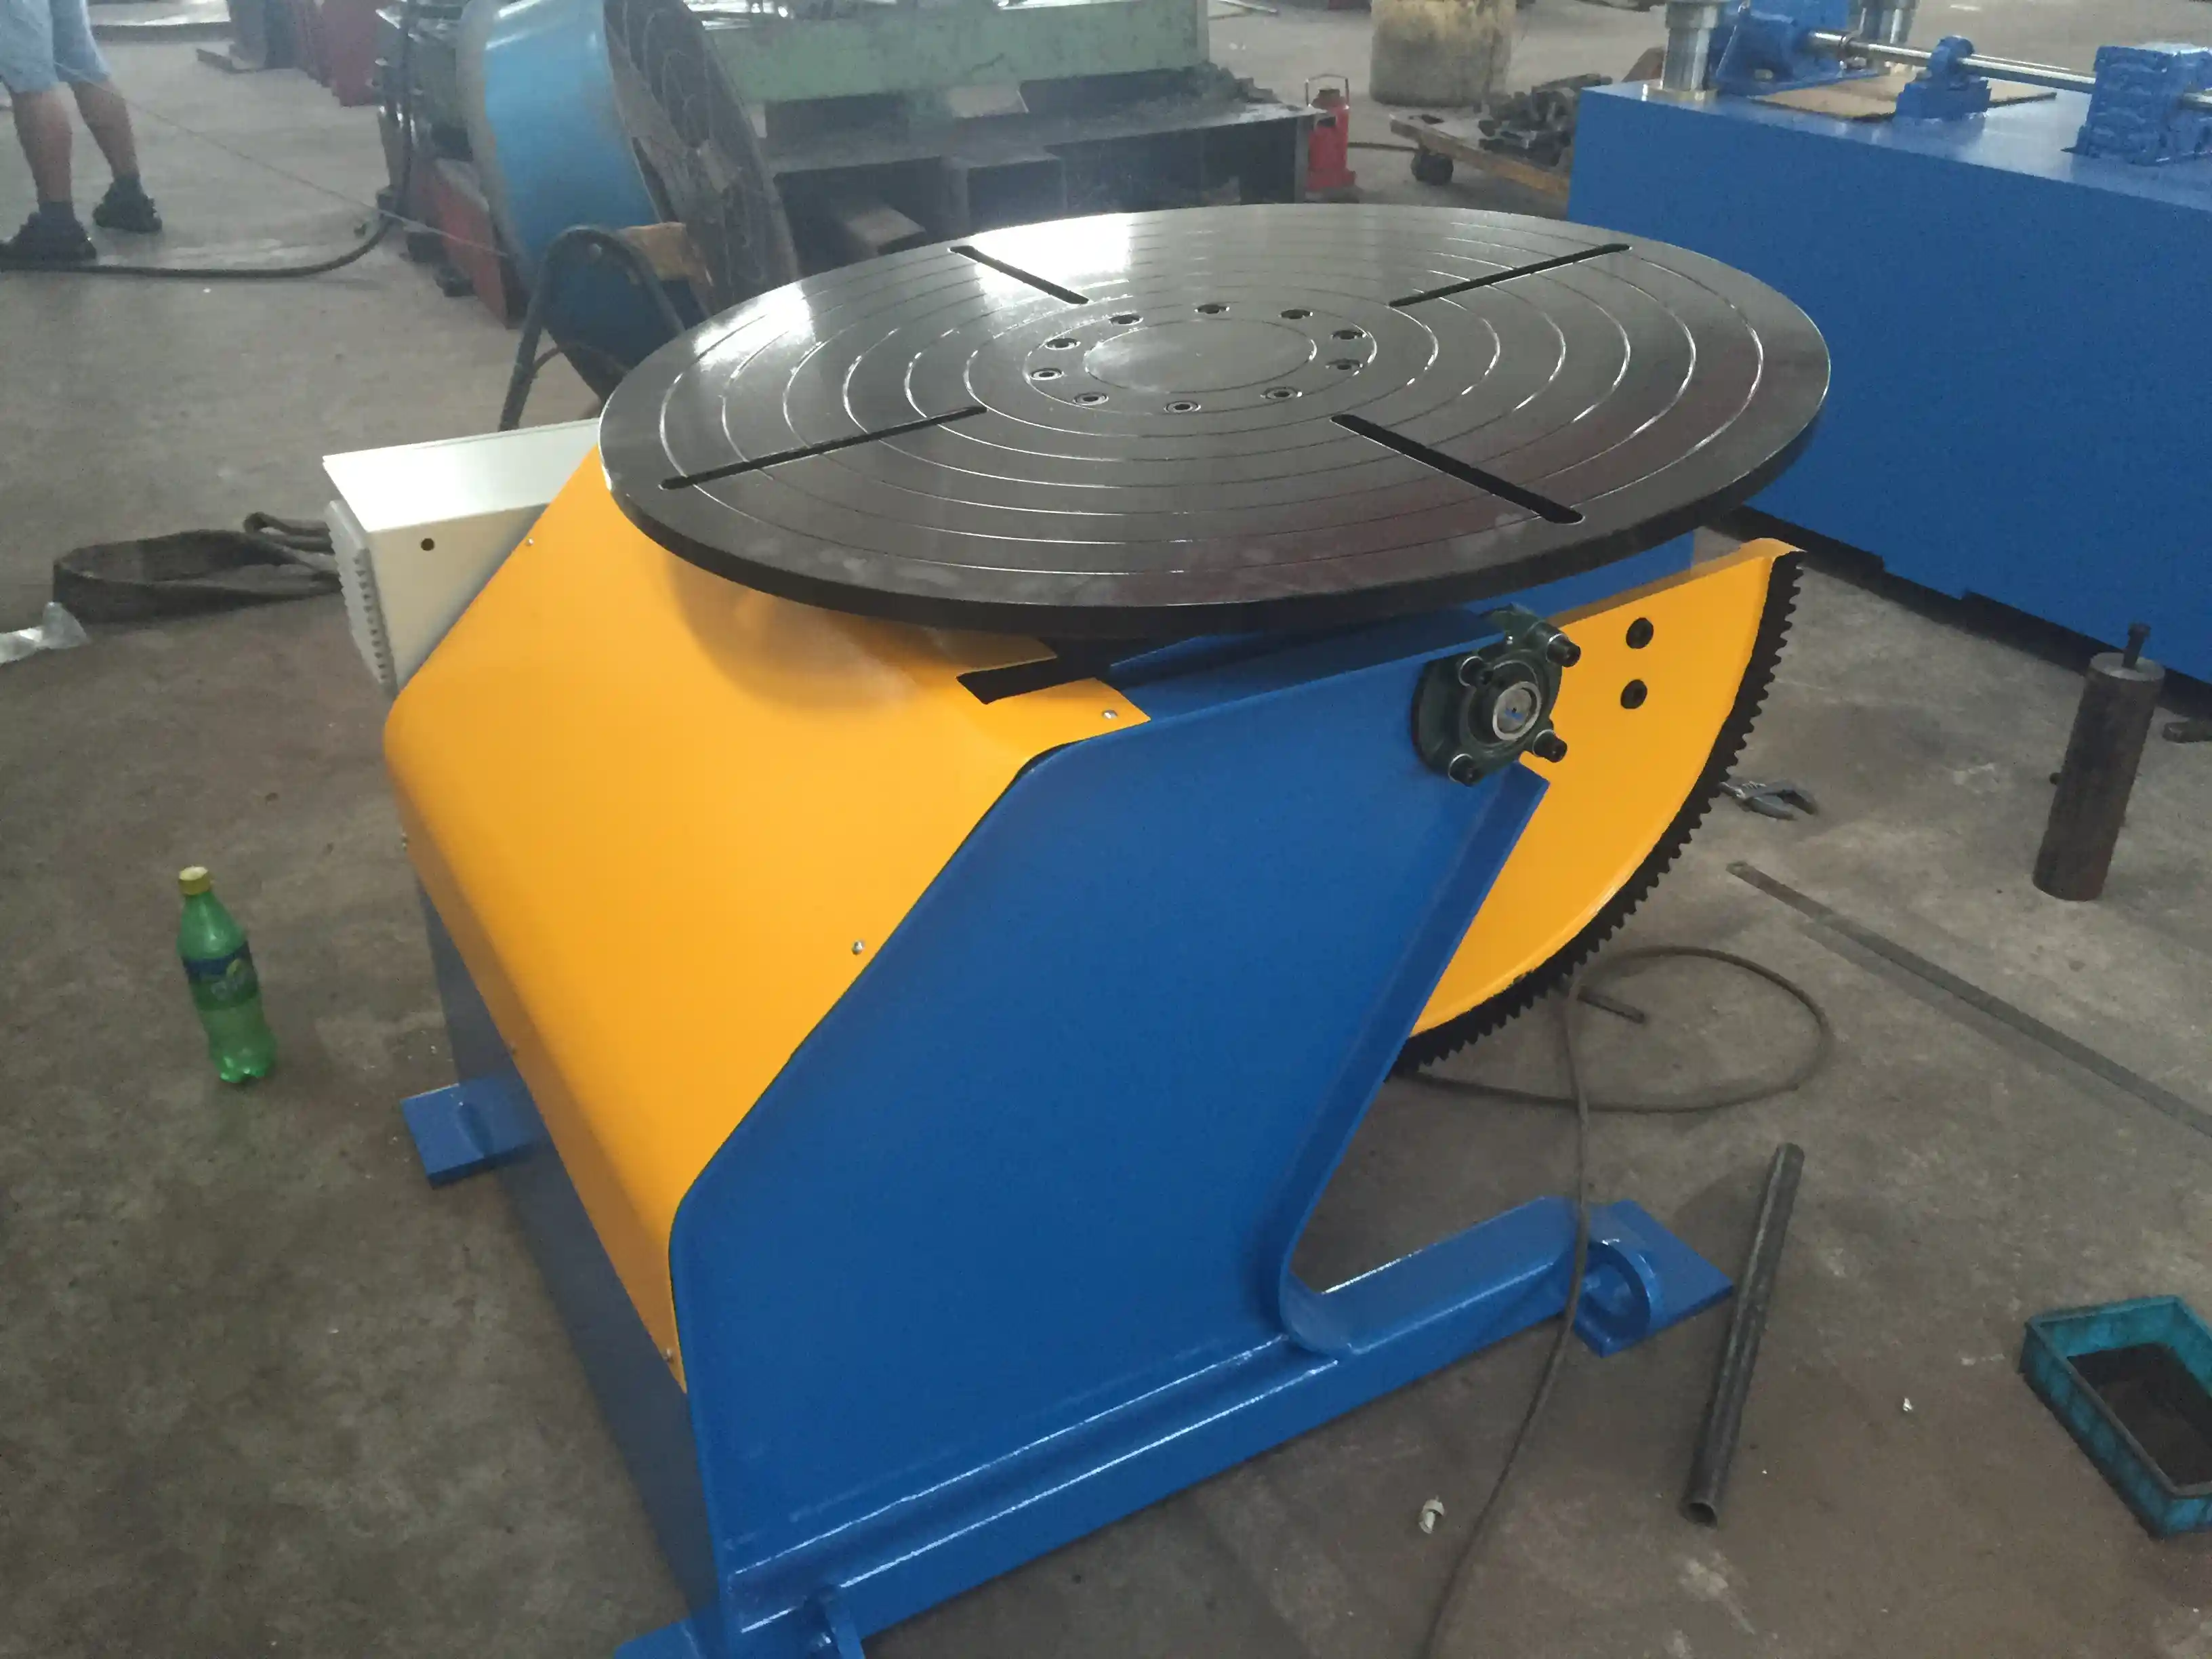
Cut blanks that move into pressure vessel, tank, or heavy structural fabrication usually need a second operation: accurate part rotation and weld positioning. If the cutting table holds a tolerance but the downstream positioner does not, the overall fit-up still suffers. This is why the cutting method and the weld-positioning stage should be evaluated together for materials above roughly 6 mm.
In many heavy-fabrication shops, water jet cutting is followed by precision positioning for weld fit-up. <Wuxi ABK Professional Welding Rotary Equipment: Precision Welding Solution for Pressure Vessel Manufacturing> covers accurate part rotation and positioning after cut preparation.
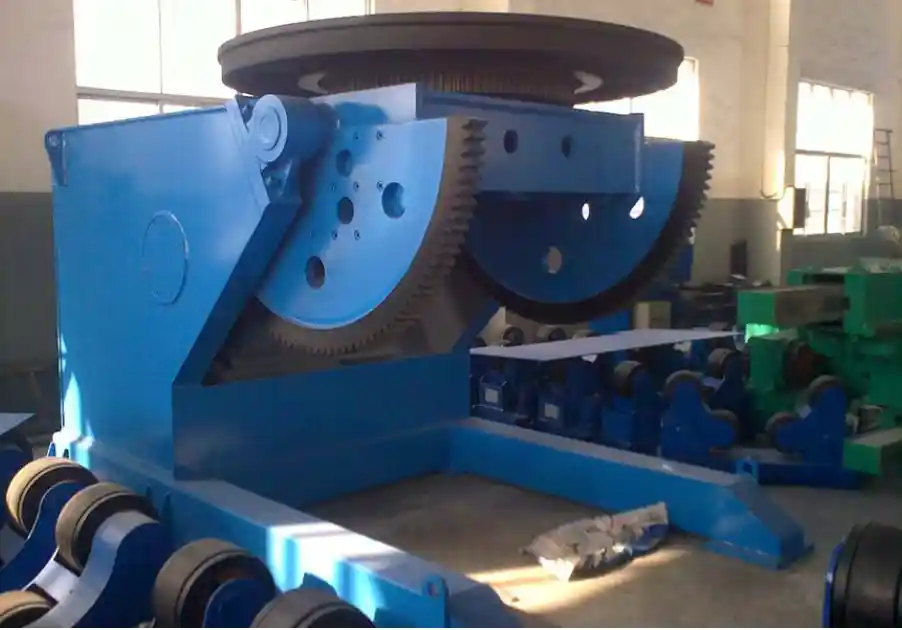
For shops that move from cut blanks into large tank or pressure vessel assembly, <Improving Quality and Efficiency in Tank and Pressure Vessel Manufacturing: The Core Application Value of Positioners> covers how rotary positioning improves the next production step.
Before requesting quotes, prepare a small technical package: sample material types and thicknesses, required tolerance, production hours per shift, and a simple sketch of the largest part footprint. That package is more useful than a general price inquiry. For a direct configuration review, send those details to jay@weldc.com. Include part drawings and monthly output so the nozzle, pump, and table options can be evaluated against the real workload.
Configuration Review for Your Material Mix
Selecting between pure water and abrasive water jet cutting is a specification problem, not just a price comparison. WUXI ABK MACHINERY CO., LTD provides CNC cutting and welding equipment for industrial fabrication lines. Contact jay@weldc.com, Tel: +86-510-83555592, or Mobile/WhatsApp: +86-13815101750 with your material list and part tolerance.
Frequently Asked Questions
What is the main difference between abrasive and pure water jet cutting?
Pure water jet cutting uses water alone to erode soft materials. Abrasive water jet cutting adds hard garnet particles into the stream, which allows the jet to cut harder and thicker materials.
Which materials require abrasive water jet cutting?
Metals, stone, glass, thick composites, and most hard engineering materials require abrasive water jet cutting. Pure water is not normally productive on those materials.
Is pure water jet cutting only for foam and food?
No. Pure water jet cutting also works for rubber, gaskets, textiles, thin plastics, and other soft materials. The process is limited by material hardness rather than by a narrow product category.
Does water jet cutting create a heat-affected zone?
Water jet cutting is widely used because it avoids the heat-affected zone associated with thermal cutting methods [1]. This makes it useful for materials or applications where heat input must be minimized.
How thick can an abrasive water jet cut?
The practical thickness depends on pump pressure, horsepower, abrasive delivery, and the material. Industrial abrasive systems routinely cut thick steel plate, stone, and layered composites, but speed decreases as thickness increases.
What is the largest operating cost difference?
Abrasive water jet cutting adds garnet consumption, mixing-tube wear, and abrasive disposal. Pure water jet cutting shifts more of the operating cost toward pump power, water filtration, and system maintenance.
Can one water jet machine cut both soft and hard materials?
Abrasive water jet machines are often used as the broad-platform choice because they can cut a wide range of materials. Pure-water operation is sometimes possible, but the nozzle and process settings must be matched correctly. For high-volume soft-material work, a dedicated pure-water machine may still be more economical.
References
[1] Water Jet Technology Association. Recommended Practices for the Use of High-Pressure Waterjetting Equipment. https://www.wjta.org
[2] Hashish, M. “Abrasive Water Jet Cutting of Materials.” Water Jet Technology Association. https://www.wjta.org
[3] Hashish, M. “Characteristics of Surfaces Machined with Abrasive-Waterjets.” Journal of Engineering Materials and Technology, ASME, vol. 113, no. 3, 1991, pp. 354–362.
If you’re interested, check out these related articles:
Pipe Rotators and Turning Rolls: Essential Equipment for Modern Pipeline Fabrication
Mastering Heavy Manufacturing: How Climbing Roller Stands Become the Cornerstone of Efficient Welding
 English
 Español
 Français
 Deutsch
 Português
 Русский