Welding positioner factories serve heavy fabrication by supplying rotation, tilting, and turning equipment that keeps large workpieces in the correct position for mechanized or manual welding. In pressure vessel, wind tower, ship, and structural steel production, reliable heavy industry solutions depend less on a single catalog number and more on how a factory manages load distribution, drive stiffness, alignment, and weld quality documentation.
What a Reliable Welding Positioner Factory Controls
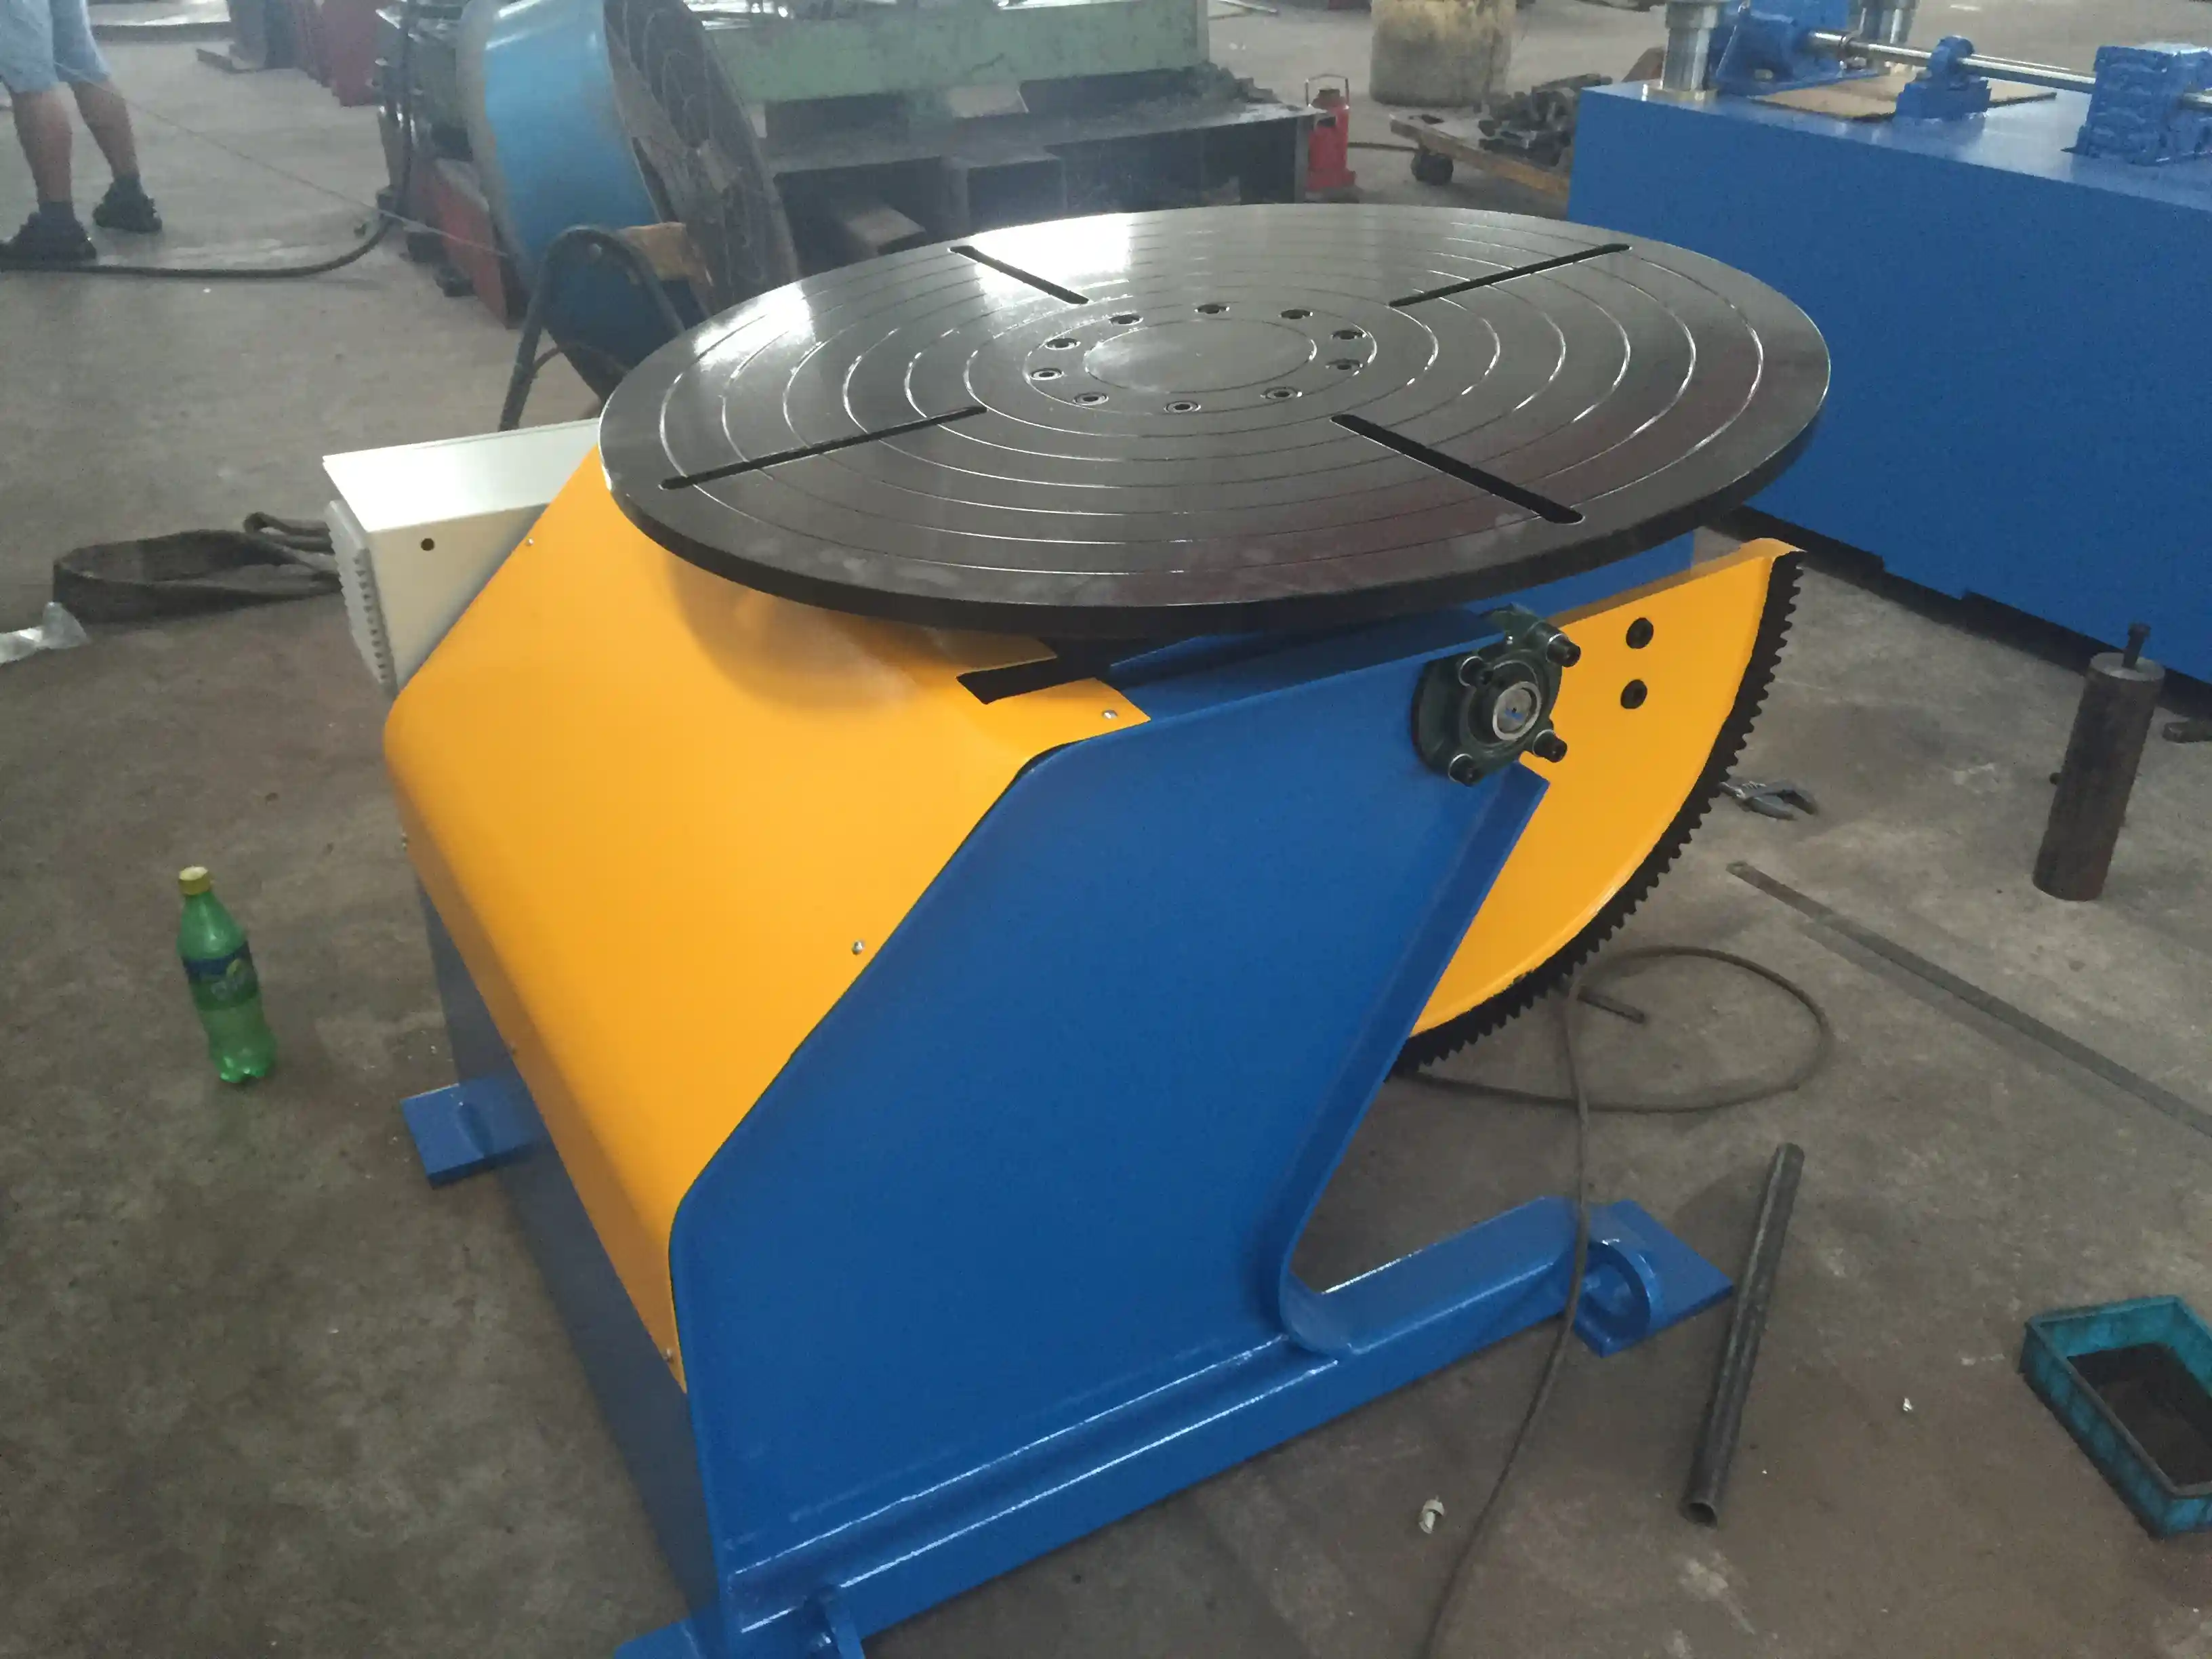
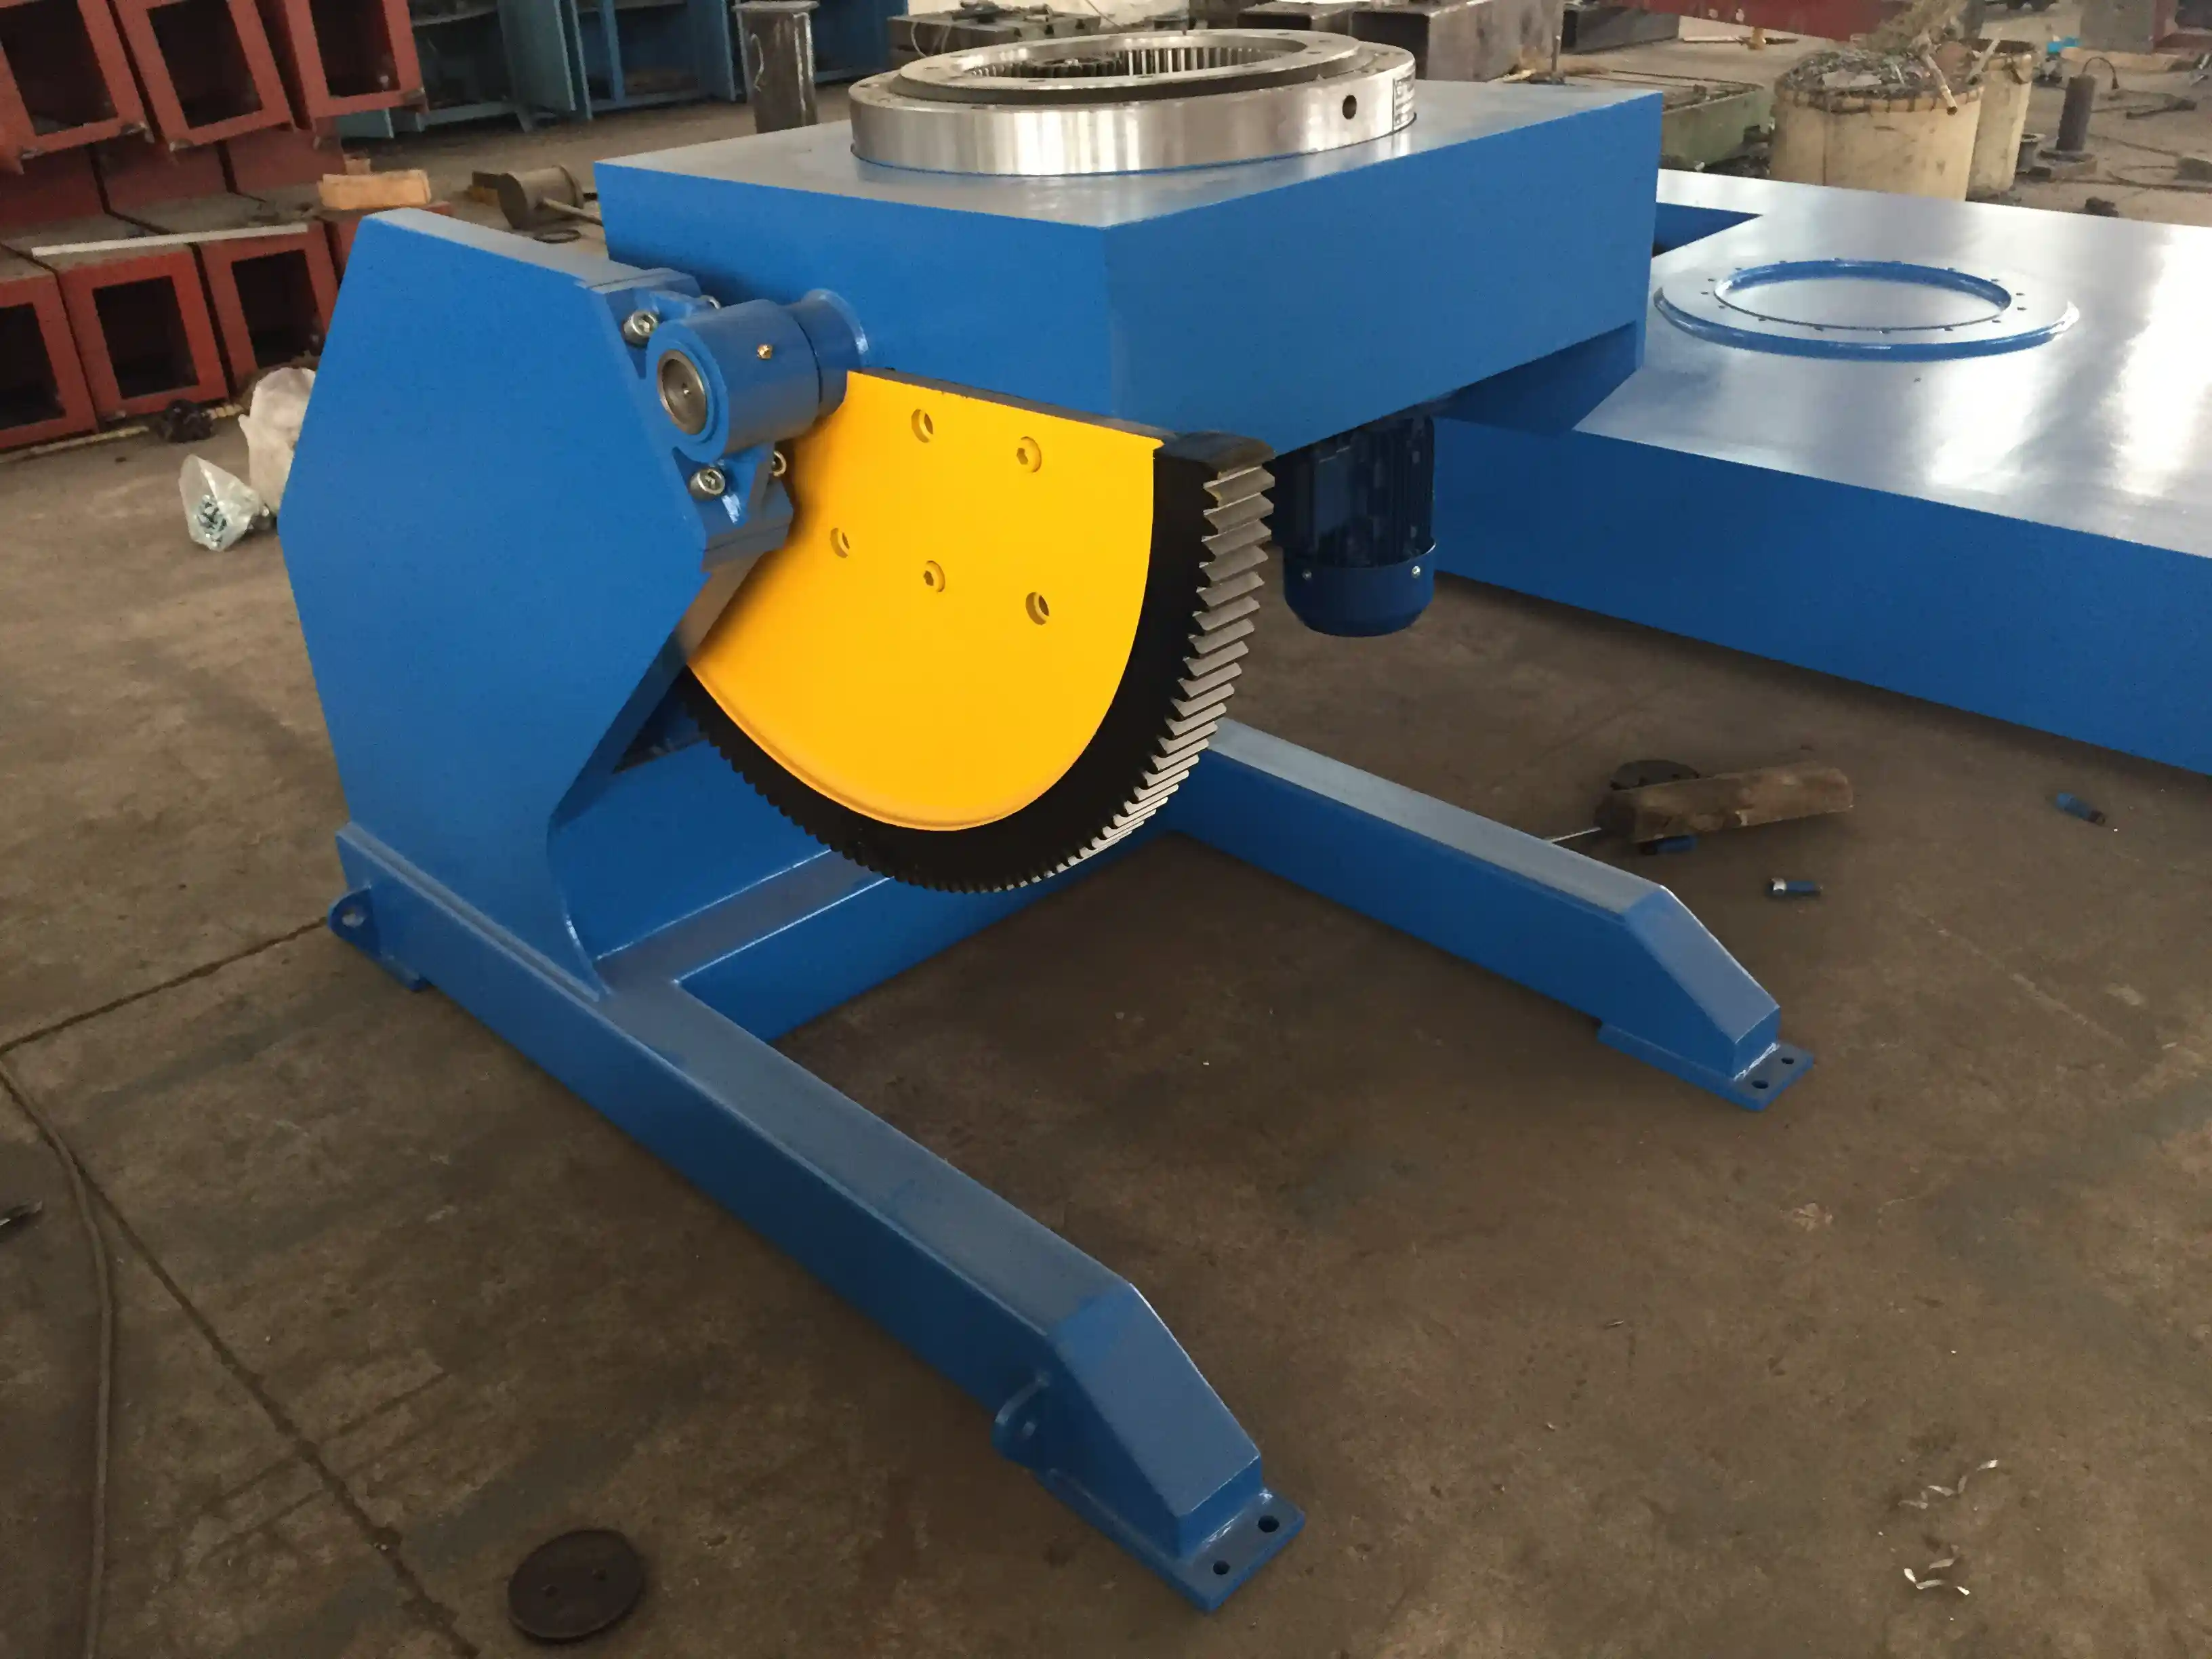
A reliable factory controls the positioner’s core mechanical path from the table to the base. The first area is load path design. A well-designed positioner transfers workpiece weight and overturning moment into a rigid frame rather than into the gearbox alone. Heavy-duty models often use a box-type or cast base, a slewing bearing, and reverse gears to handle axial, radial, and overturning loads. Product records for fixed-height and adjustable-height units commonly list both load capacity and maximum eccentric distance because eccentric loading changes the effective demand on the drive system.
The second area is motion accuracy. For heavy welding, a positioner should maintain consistent rotation speed and return the worktable to the same orientation within a defined tolerance. Standard fixed-height positioners often specify rotation accuracy of about ±0.5°, while 3-axis servo-driven tables may list positioning accuracy of ±0.05 mm because they are intended for robotic cells and precision components. Buyers should compare accuracy values only with the intended welding process; a ±0.05 mm positioner is not automatically required for every heavy structural weld.
The third area is control integration. PLC and HMI systems allow preset programs, adjustable rotation speed, and communication with robotic systems. For automated heavy fabrication, the positioner should be able to accept start, stop, speed, and position commands from the welding cell controller.
Positioner Configurations for Heavy Loads
Heavy industry projects use different positioner configurations depending on workpiece shape, weight, and required weld position.
| Positioner configuration | Common load range | Typical heavy-industry use | Key selection factor |
|---|---|---|---|
| Fixed-height L-type | 1–100 t | Pressure vessels, excavator booms, crane segments | Center-of-gravity distance and table flatness |
| Adjustable-height | 5–100 t | Wind tower sections, long vessels, structural steel | Hydraulic lifting range and anti-creep control |
| 3-axis precision | 1–5 t | Robotic MIG/TIG welding cells, aerospace components | Servo accuracy and robot compatibility |
| Head-tail | 1–3 t | Long pipe, shaft, rail and machinery components | Distance between bases and workpiece length |
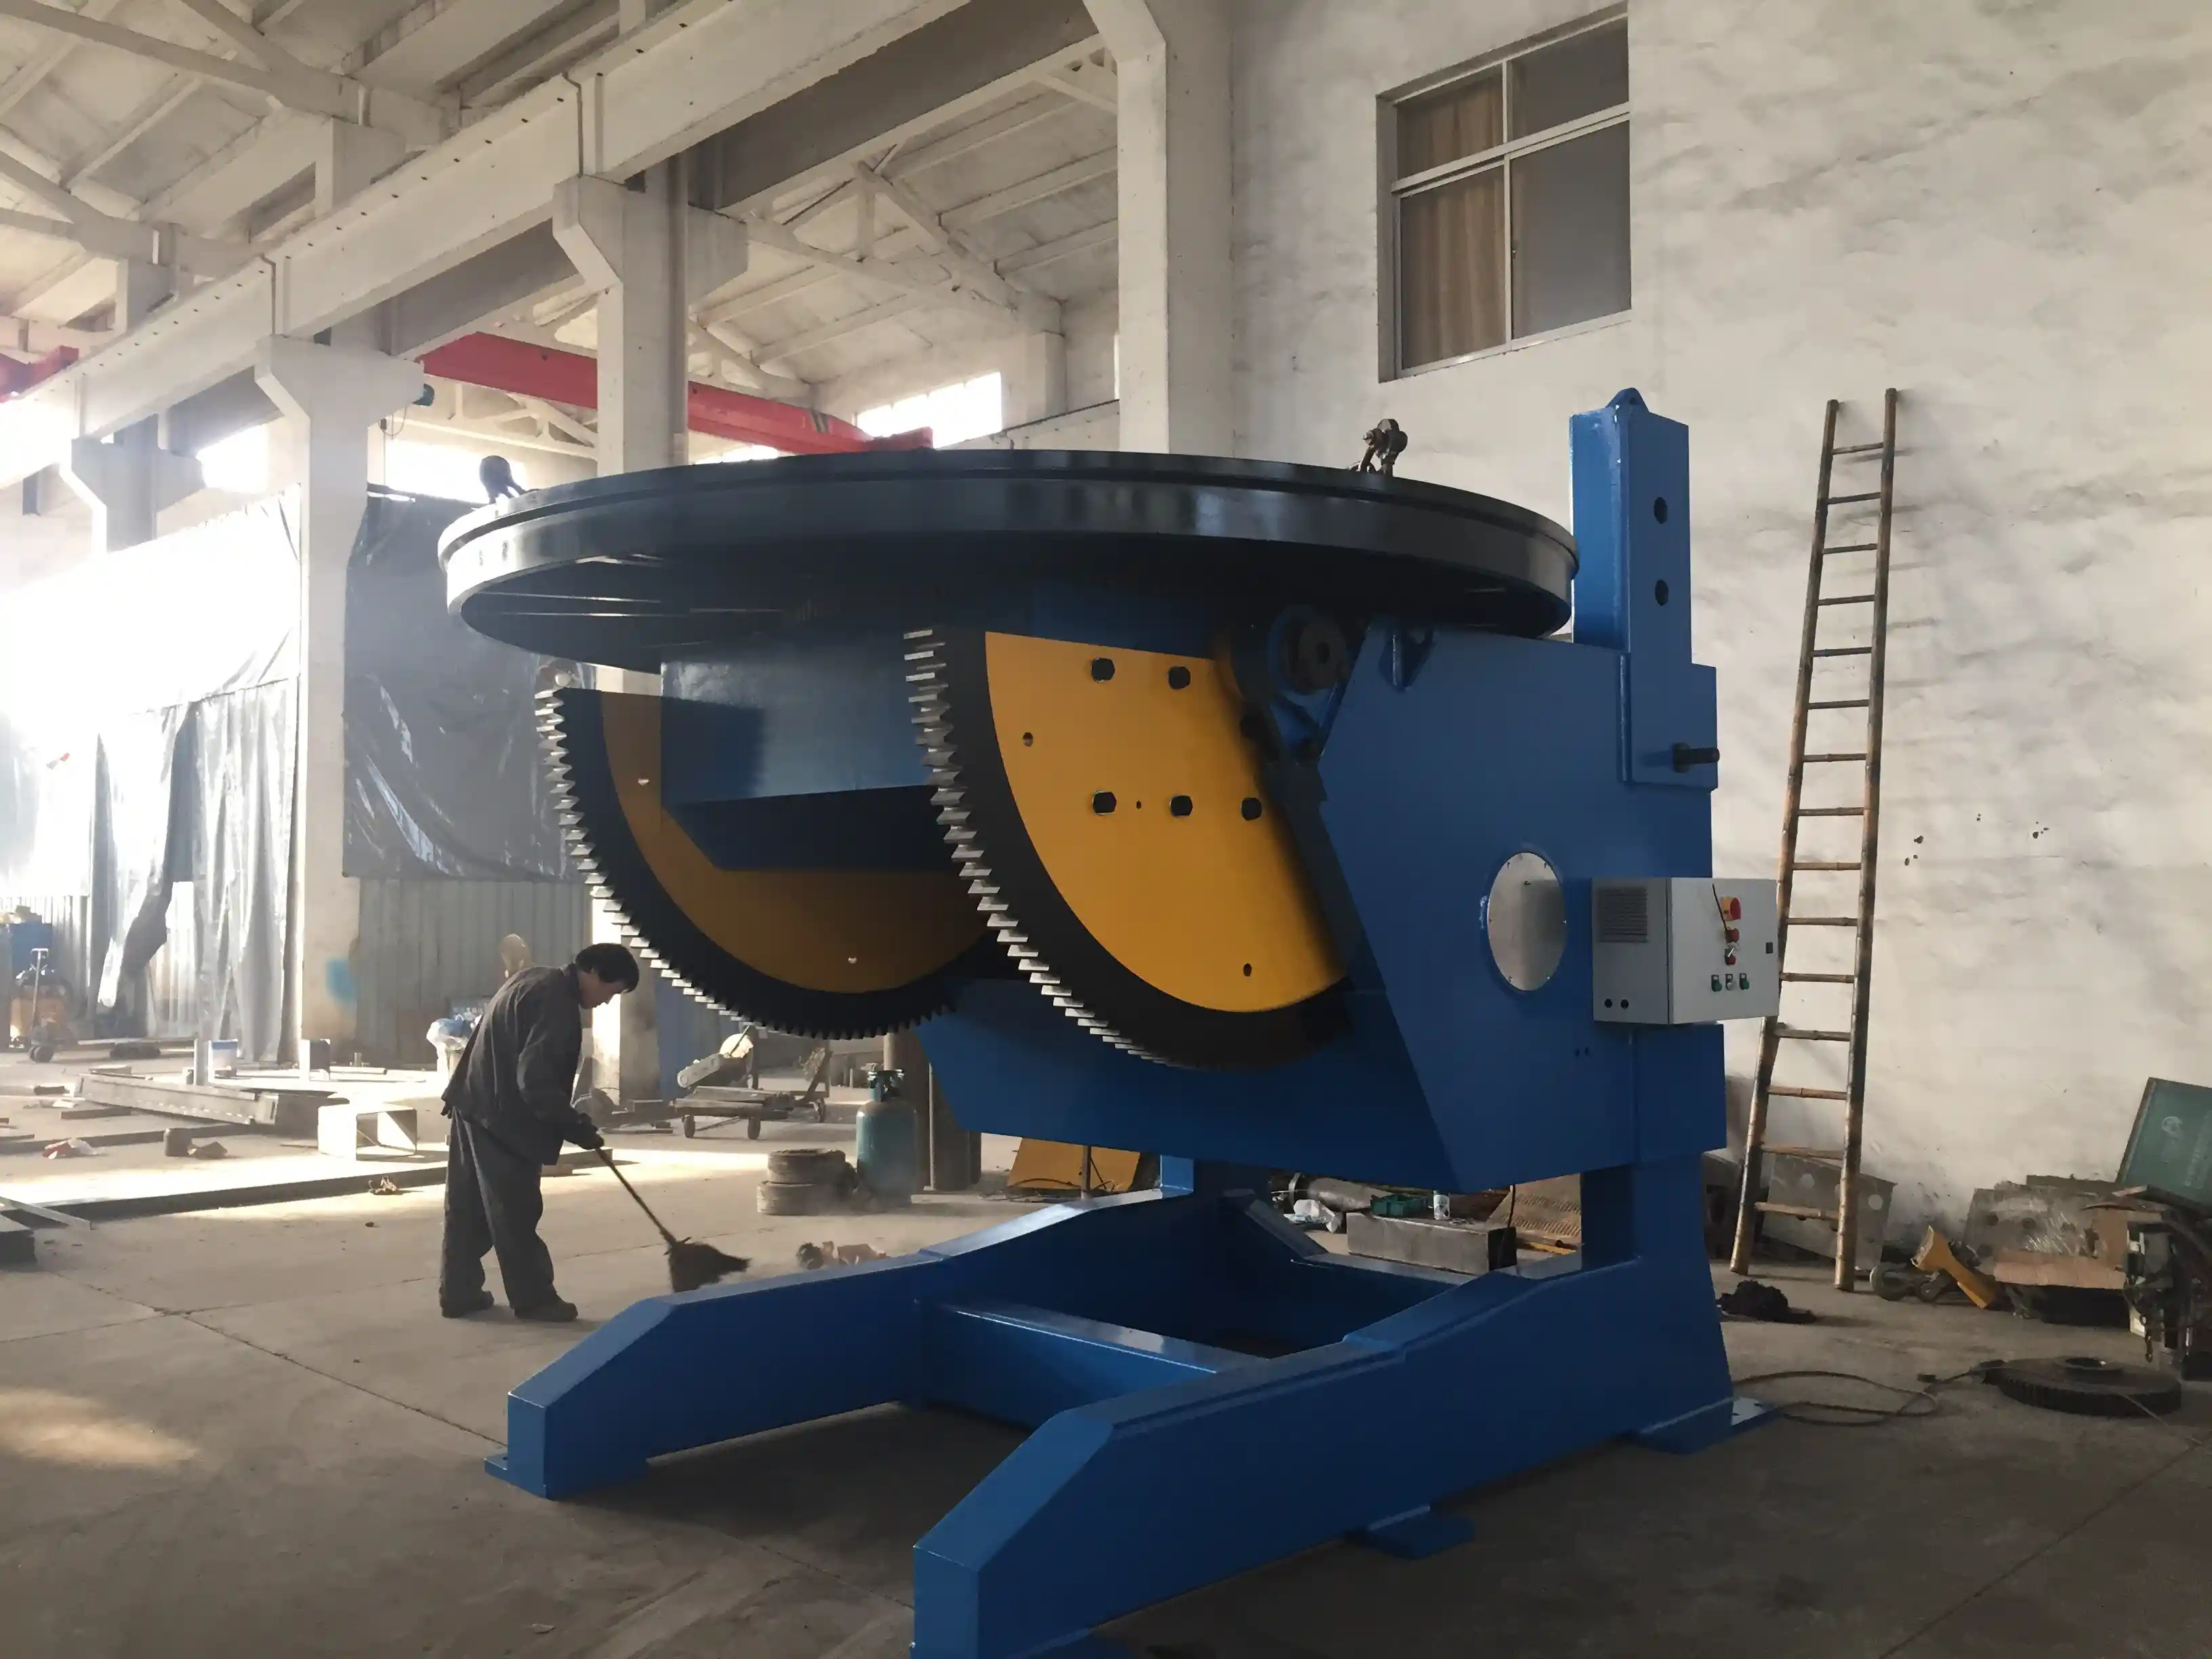
Fixed-height L-type positioners are common in heavy fabrication because they provide a stable table and a simple tilt path. Adjustable-height machines add flexibility when the same bay must serve different vessel diameters or floor conditions. A Posicionador de soldadura de 3 eixos is most useful when the workpiece must move through several coordinated orientations under robot control. For large-diameter shell work, an Posicionador de soldadura ajustável can position the seam at a height that matches the manipulador de soldadura boom.
Quality Systems and Welding Code Alignment
A factory is not reliable only because it supplies a rotating table. It must also support the welding quality system around the equipment. EN ISO 14731 [1] assigns responsibilities for welding coordination activities, from procedure qualification to inspection planning. For structural steel fabrication, AWS D1.1 [2] establishes requirements for qualified welding procedures and workmanship. Pressure-retaining components often fall under ASME BPVC Section IX [3], which covers welding procedure and performance qualification. ISO 3834-2 [4] provides a comprehensive quality framework for fusion welding, including equipment condition and maintenance as part of the production system.
When evaluating a welding positioner factory, ask for evidence that its equipment supports weld qualification and inspection records. The positioner itself is part of the production process, so calibration records, runout checks, and drive-speed verification should be included with machine acceptance. A factory operating under a certified quality management system such as ISO 9001 [5] should be able to supply documented inspection data and traceable component records.
Heavy-Load Applications That Expose Factory Quality
Pressure vessels and tanks are among the strongest test cases for a welding positioner factory. A vessel shell must rotate at a controlled speed while the welding head stays on the seam centerline. If the table deflects or the drive speed varies, deposition rate and bead shape change. Large-diameter shells also present high overturning loads, especially when the shell is offset or partially filled with fixturing.
For pressure vessel and tank fabrication, positioner performance directly affects roundness control and pass rates. <Melhorar a Qualidade e a Eficiência no Fabrico de Reservatórios e Recipientes sob Pressão: O principal valor de aplicação dos posicionadores> covers how load distribution, table flatness, and rotation stability influence heavy-shell welding.
Wind tower fabrication adds length and diameter challenges. Tower sections often require coordinated rotation with a welding manipulator or column boom, and the positioner must resist axial drift during longitudinal and girth welding. The table should rotate smoothly at low speeds, and the tilt or turning function should provide access for flange, door frame, and internal bracket welds.
Ship and offshore structural welding also depends on positioner stiffness. Large curved panels, hull subassemblies, and pipe spools may need to be rotated to maintain flat or horizontal groove positions. In ship welding, controlled rotation and tilt improve access and reduce the amount of overhead welding required.
In ship welding, positioners are used to reduce overhead and vertical-position work. <Revolução na soldadura naval: como os posicionadores de soldadura melhoram a qualidade e a eficiência> covers how controlled rotation and tilt improve access and deposition consistency for large structural components.
Key Specification Data to Request
To compare welding positioner factories, request more than the rated capacity. The following data set separates a qualified heavy-industry supplier from a generic machine builder:
- Maximum load and center-of-gravity distance, not just table capacity.
- Rotation speed range and speed regulation method.
- Tilt or turnover angle range.
- Worktable diameter, T-slot layout, and maximum rotating diameter at 90° overturn.
- Position accuracy and repeatability for servo-driven axes.
- Drive type, reducer type, and slewing bearing details.
- Control system interface and robot compatibility.
- Lifting range and adjustment method for adjustable-height machines.
- Safety functions: emergency stop, overload protection, anti-fall pins, and enclosure rating.
- Factory acceptance and calibration records.
Need a starting configuration for your workpiece? Send the load, table diameter, tilt angle, and material thickness to jay@weldc.com for a technical comparison.
Building a Heavy Industry Sourcing Checklist
When comparing welding positioner factories, use a structured checklist to avoid over-weighting price. First, confirm that the factory understands the application-specific load condition. A 10-ton load centered on the table is not the same as a 10-ton load offset by 200 mm. Second, ask how the machine maintains speed under changing load. Third, verify that the factory can provide pre-shipment inspection data. Fourth, review the control architecture for future automation integration. Finally, match the positioner to the welding manipulator or robot interface, so the complete cell operates as one system.
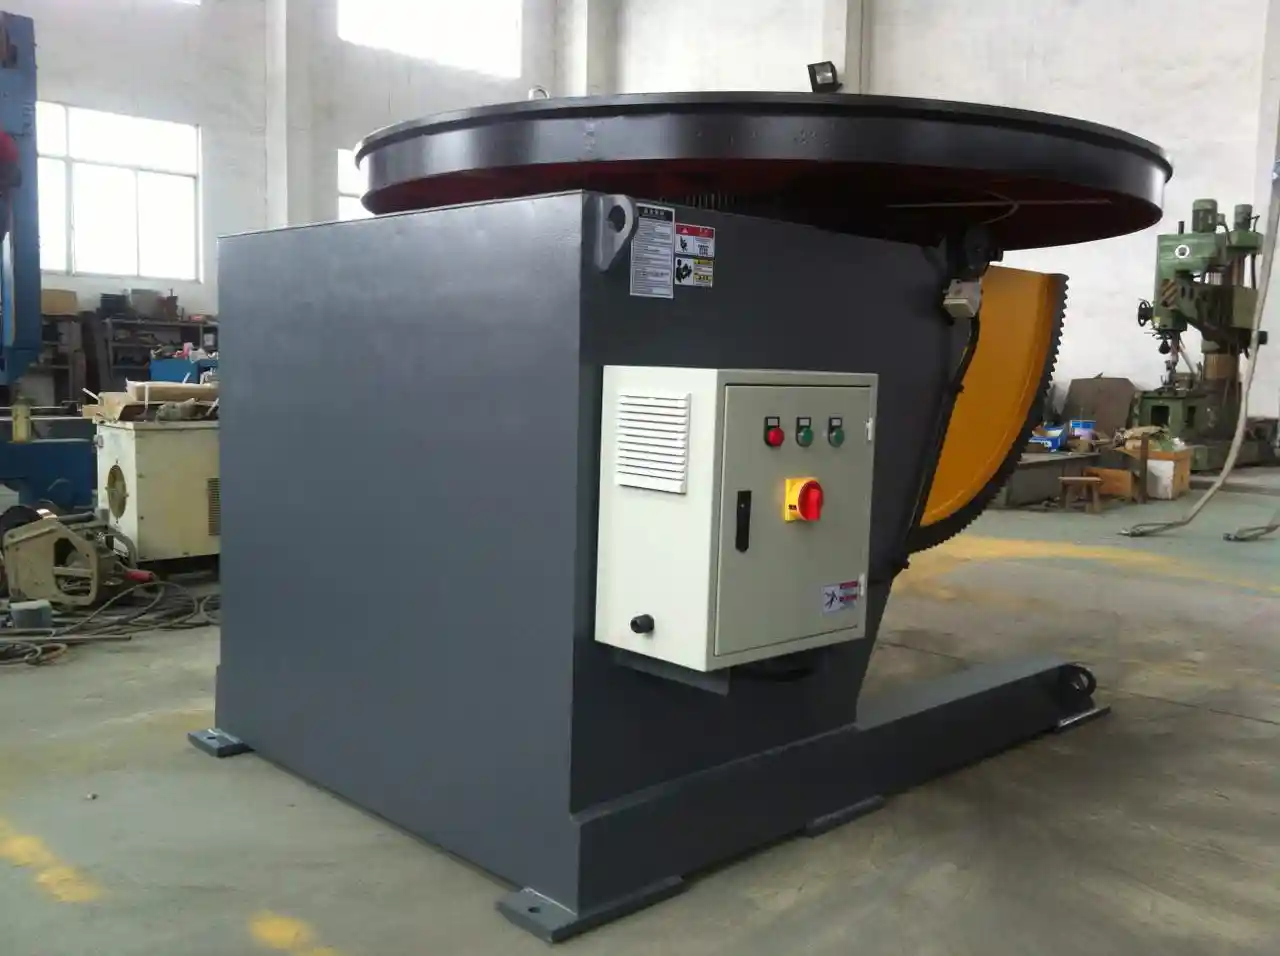
For buyers that need a flexible heavy fabrication cell, a Soluções para mesas giratórias de soldadura platform can cover many medium-duty rotating and tilting tasks. For long vessel and tower sections, pairing an adjustable-height positioner with a welding manipulator usually provides better centerline control than relying on the positioner alone.
Request a Heavy Industry Positioner Inquiry
For project-specific sizing, contact WUXI ABK MACHINERY CO., LTD with your workpiece weight, dimensions, and welding process.
- Tel: +86-510-83555592
- Telemóvel: +86-13815101750
- Fax: +86-510-83559158
- Correio eletrónico: jay@weldc.com
Perguntas mais frequentes
How do I choose between fixed-height and adjustable-height welding positioners?
Choose fixed-height when the production bay is dedicated to a narrow range of workpiece diameters and table height stays consistent. Choose adjustable-height when the same cell must handle multiple vessel diameters, varying weld head heights, or workpieces that require frequent setup changes. Hydraulic lifting and anti-creep control are more important on high-tonnage adjustable machines.
What load rating should I specify?
Specify the total workpiece weight, the maximum eccentric distance, and the center-of-gravity distance. The rated load alone is not enough. If the load is offset, the effective overturning moment may exceed the drive and bearing capacity even when total weight remains inside the nominal tonnage.
Which standards apply to pressure vessel or structural welding positioners?
The positioner itself is usually not the certified weld procedure, but it must support the production system. For structural steel, AWS D1.1 [2] applies to the welding procedure and workmanship. For pressure-retaining welds, ASME BPVC Section IX [3] governs procedure and performance qualification. ISO 3834-2 [4] addresses manufacturing quality requirements for welding, including equipment suitability.
How do factories verify positioner accuracy before shipment?
Request factory acceptance records that show table runout, rotation speed tolerance, tilt range, and repeatability for servo-driven axes. A load test or no-load run with documented measurements is more useful than a general certificate. For precision 3-axis machines, ask for positioning accuracy and repeatability data.
What maintenance should a heavy-duty positioner receive?
Daily maintenance should include removing welding spatter, checking lubrication, and inspecting electrical connections. Monthly or quarterly tasks usually include bolt torque checks, gear and drive inspection, and safety interlock testing. Annual work should cover bearing and seal replacement, re-lubrication, and recalibration of positioning accuracy if required.
References
[1] EN ISO 14731:2019, Welding coordination — Tasks and responsibilities.
[2] AWS D1.1/D1.1M:2020, Structural Welding Code—Steel.
[3] ASME BPVC Section IX:2023, Qualification Standard for Welding, Brazing, and Fusing Procedures.
[4] ISO 3834-2:2021, Quality requirements for fusion welding of metallic materials — Part 2: Comprehensive quality requirements.
[5] ISO 9001:2015, Quality management systems — Requirements.
Se estiver interessado, consulte estes artigos relacionados:
Solução revolucionária para a soldadura de vasos de pressão: Análise técnica de posicionadores de soldadura rotativos de 360 graus
Dominar a produção pesada: Como os suportes de rolos trepantes se tornam a pedra angular de uma soldadura eficiente
Melhorar a Qualidade e a Eficiência no Fabrico de Reservatórios e Recipientes sob Pressão: O principal valor de aplicação dos posicionadores
Rotadores de tubos e rolos de torneamento: Equipamento essencial para o fabrico moderno de condutas
Aplicações inovadoras de rotores de soldadura CNC de 10 toneladas no fabrico de recipientes sob pressão
 English
 Español
 Français
 Deutsch
 Português
 Русский