
Choosing between a manipulador de soldadura and a welding positioner usually comes down to one decision: should the welding head move, or should the workpiece move? Both types of equipment reduce manual handling, stabilize weld parameters, and improve repeatability, but they solve different problems on the shop floor. Understanding that difference before specifying a machine prevents a mismatched automation investment.
A manipulator provides a guided, powered path for the welding torch. A positioner presents the part to the torch in the correct orientation. In high-mix heavy fabrication, the most productive cells often combine both, but the decision still begins with the primary bottleneck: long seam travel or difficult part orientation.
Core Difference: The Welding Head vs. the Workpiece
A welding manipulator is a column and boom system that carries the welding head along horizontal and vertical axes. It controls torch-to-work distance, travel speed, and vertical position during welding. This is especially useful for long longitudinal seams, tank courses, beam flanges, and other joints where the part is too large to rotate or reposition repeatedly. The manipulator moves the tool; the workpiece remains stationary or is rotated separately by turning rolls.
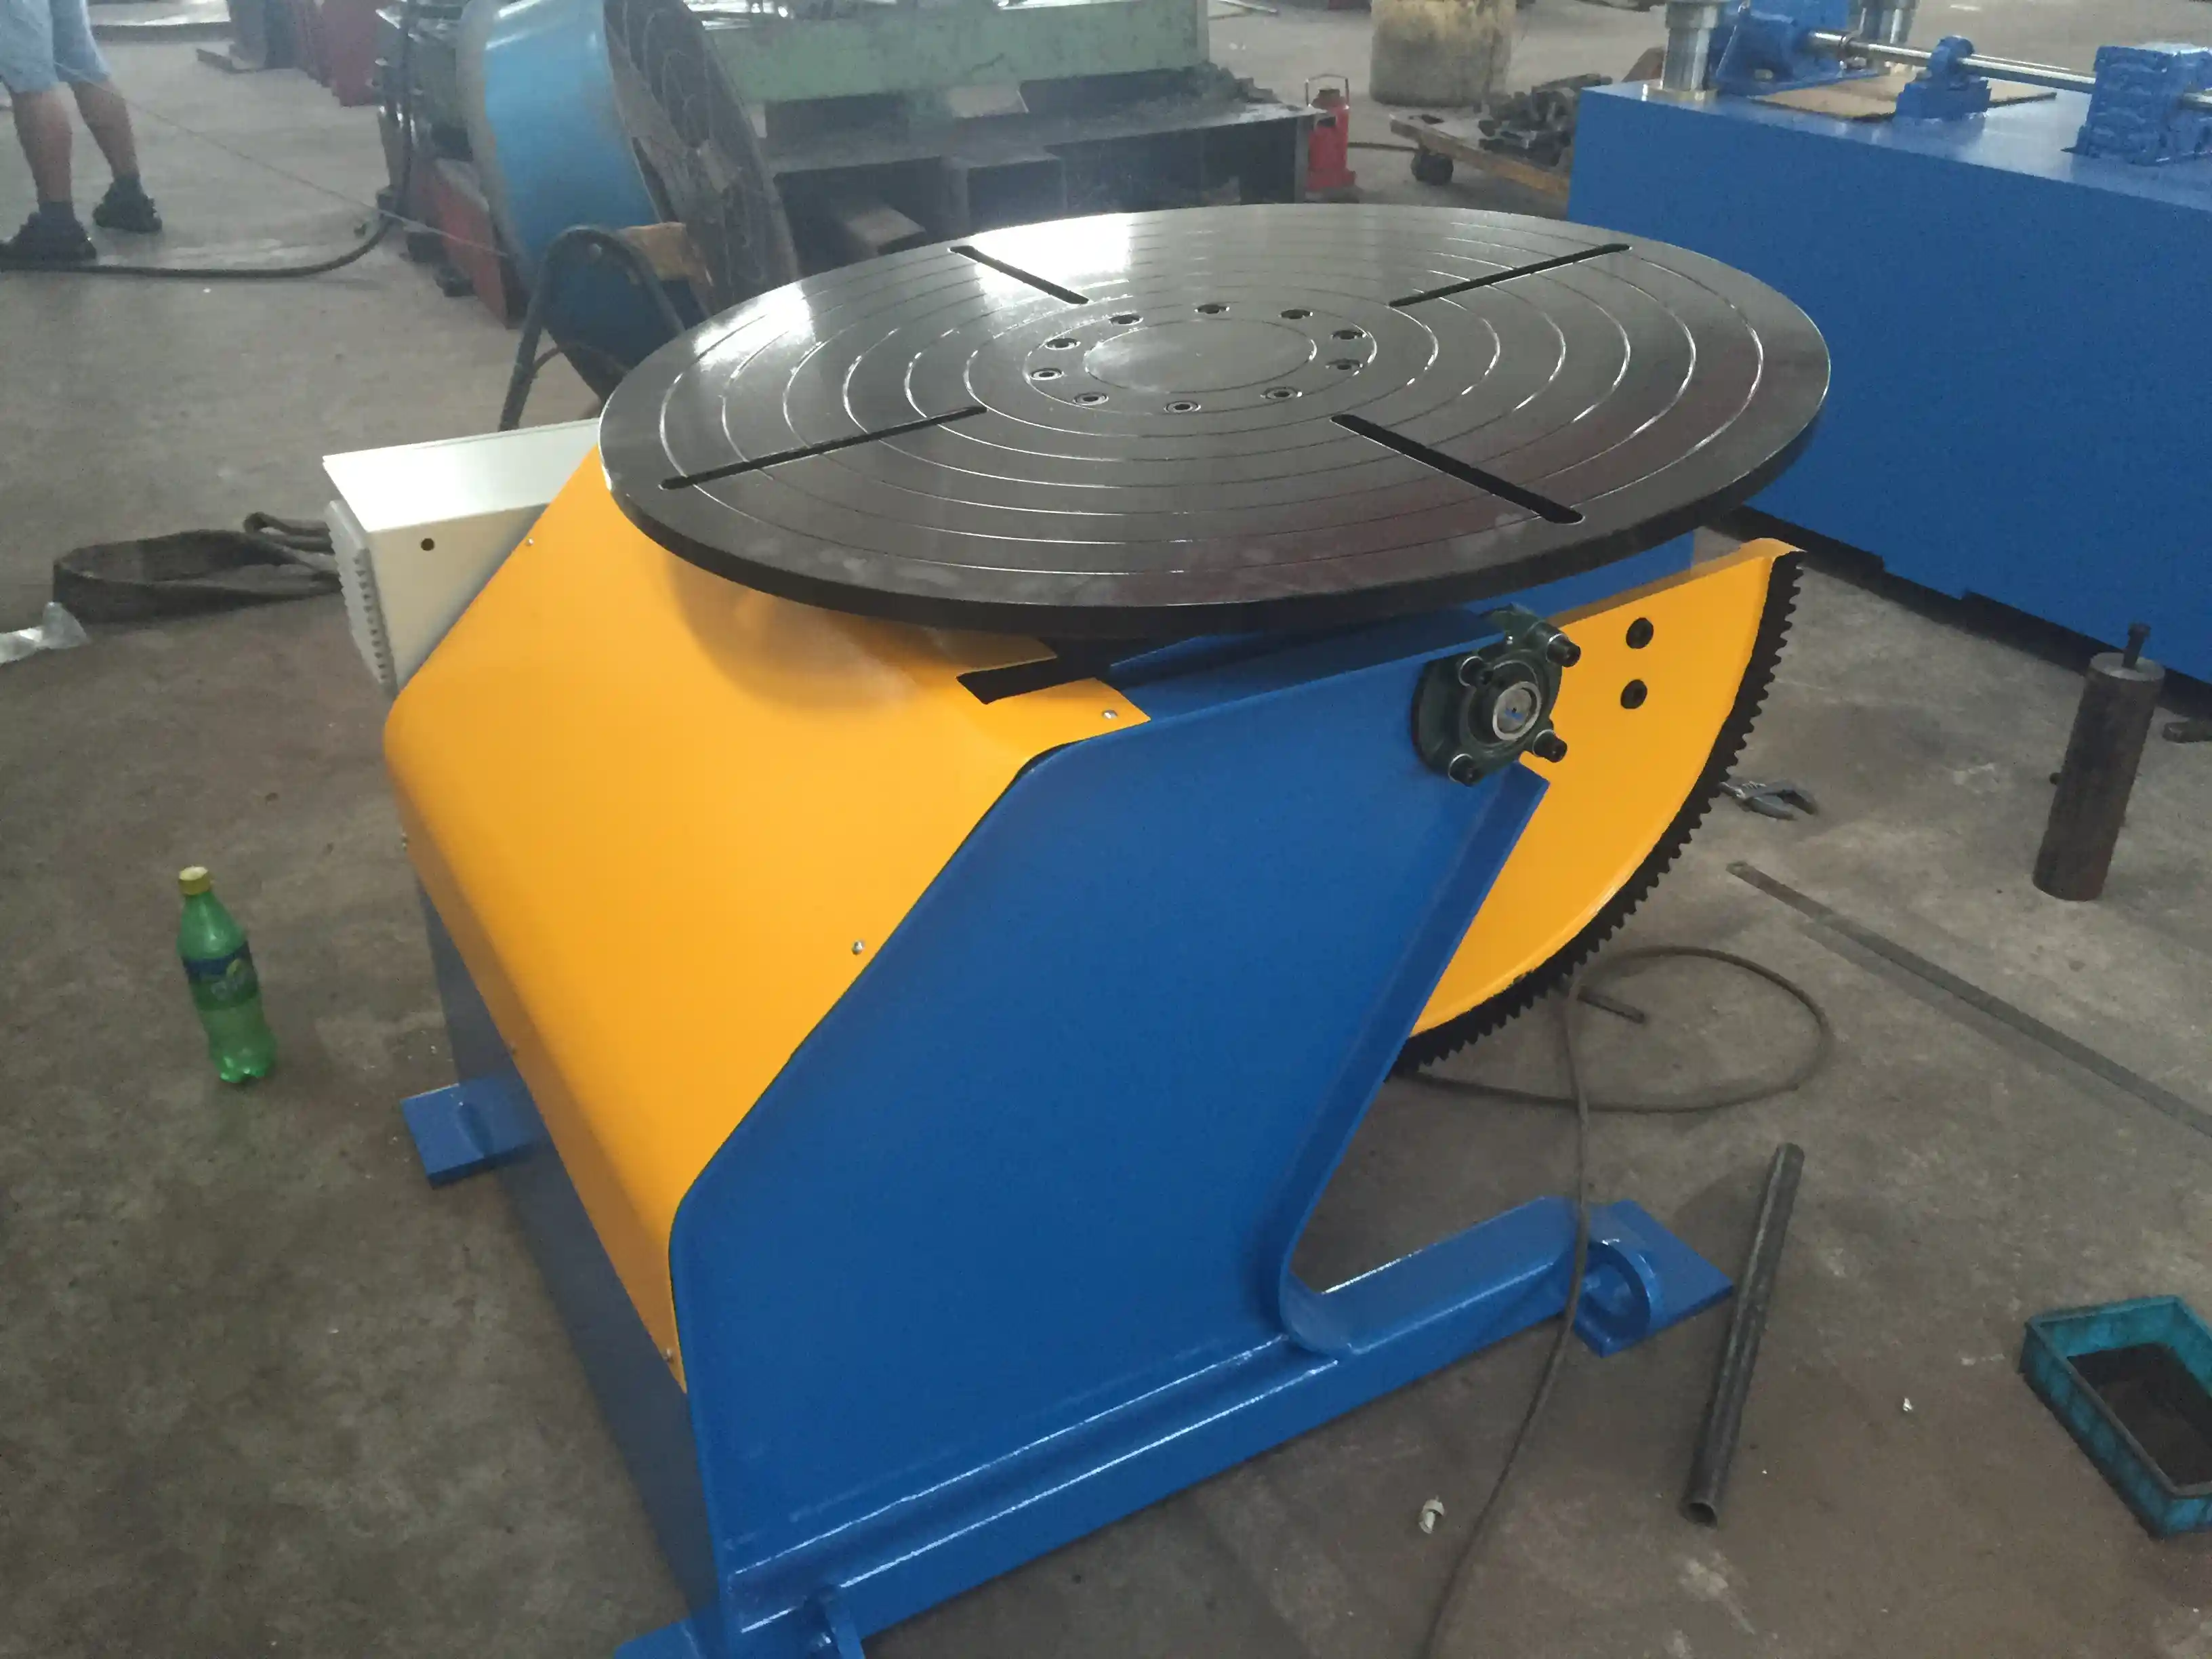
A welding positioner grips the workpiece and rotates, tilts, or turns it so that the weld joint stays in the flat, horizontal, or otherwise qualified position[1]. Positioners are built around the workpiece, not the seam. A 3-axis positioner can rotate 360° continuously, tilt from 0° to 90°, and turn the table, allowing the operator to keep the welding puddle in a favorable position even as the part geometry changes.
| Fator | Manipulador de soldadura | Posicionador de soldadura |
|---|---|---|
| Primary motion | Moves welding head/boom | Rotates, tilts, or turns workpiece |
| Best joint | Long straight or circumferential seams | Girth, flange, multi-position welds |
| Workpiece mass | Not directly supported | Directly loaded on table or fixturing |
| Typical automation | SAW, MIG, TIG carriage | Robotic MIG/TIG/SAW cell |
| Reach requirement | Boom travel and rail length | Load capacity and center-of-gravity offset |
| Orientation control | Torch angle and travel speed | Flat/horizontal weld position |
This distinction is not absolute. A long tank shell may use a manipulator for the longitudinal seam and turning rolls for the circumferential seam. But if only one machine is being added, the joint geometry usually tells you which motion is missing.
When a Welding Manipulator Works Best
Use a welding manipulator when the weld path is long and the workpiece is heavy, awkward, or expensive to move. Wind tower sections, H-beam assemblies, large storage tank shells, and heavy structural members all benefit from a boom-mounted head that travels along the joint. Common manipulator configurations provide 1,200 mm to 8,000 mm of horizontal boom travel and 3,500 mm to 8,000 mm of vertical travel, with rail-mounted carriages for extended seam coverage. That reach reduces crane moves and keeps travel speed steadier than manual carriage handling.
The manipulator is particularly effective for submerged arc welding on long joints. It carries the wire feeder, flux delivery system, and control pendant in one place while the column guides the torch. Because the machine maintains a preset arc length and travel speed, it reduces stops, starts, and uneven penetration caused by operator fatigue or hand-held torch movement.
For long tower sections and heavy fabrications, the manipulator reduces crane moves and manual repositioning. <Manipuladores de soldadura para o fabrico de torres eólicas: Revolucionando a eficiência da produção> covers how column-boom systems improve longitudinal weld productivity in wind tower production.
A manipulator can also support circumferential welding when paired with turning rolls or a rotator. The head stays at the seam while the vessel rotates under it. This is a standard production approach for tank and pressure vessel courses, because the machine can weld both the longitudinal and girth seams without moving the workpiece between separate stations.
When a Welding Positioner Is the Better Fit
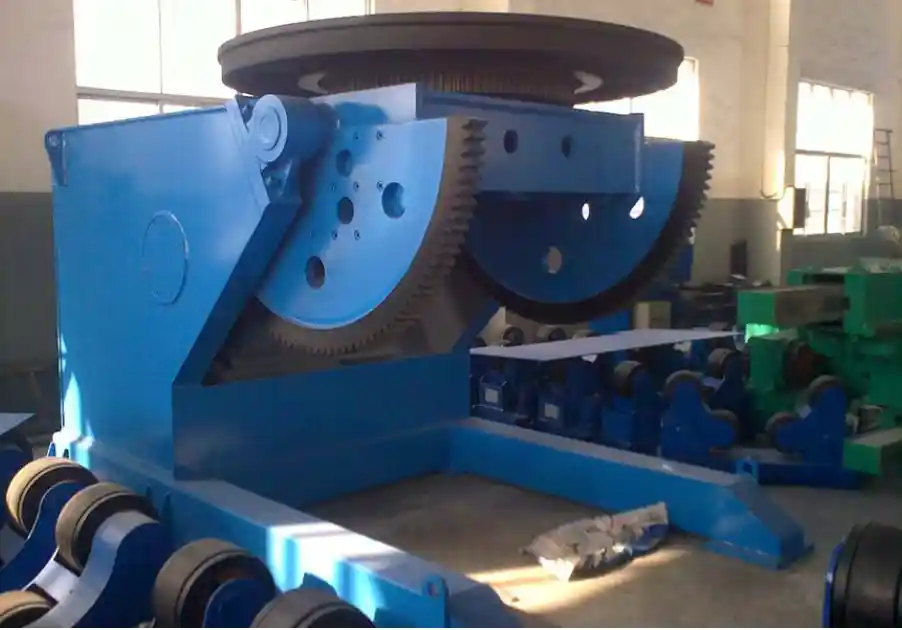
A positioner is usually the better choice when the part benefits from being repositioned rather than the torch traveling a long path. Pipe flanges, elbows, valve bodies, excavator arms, crane segments, rail bogies, and pressure vessel heads can be rotated so the weld puddle stays in the flat or horizontal position[1]. Tilting the part helps the weld pool solidify evenly and can reduce defects such as slag inclusions, undercut, and lack of fusion on complex joints.
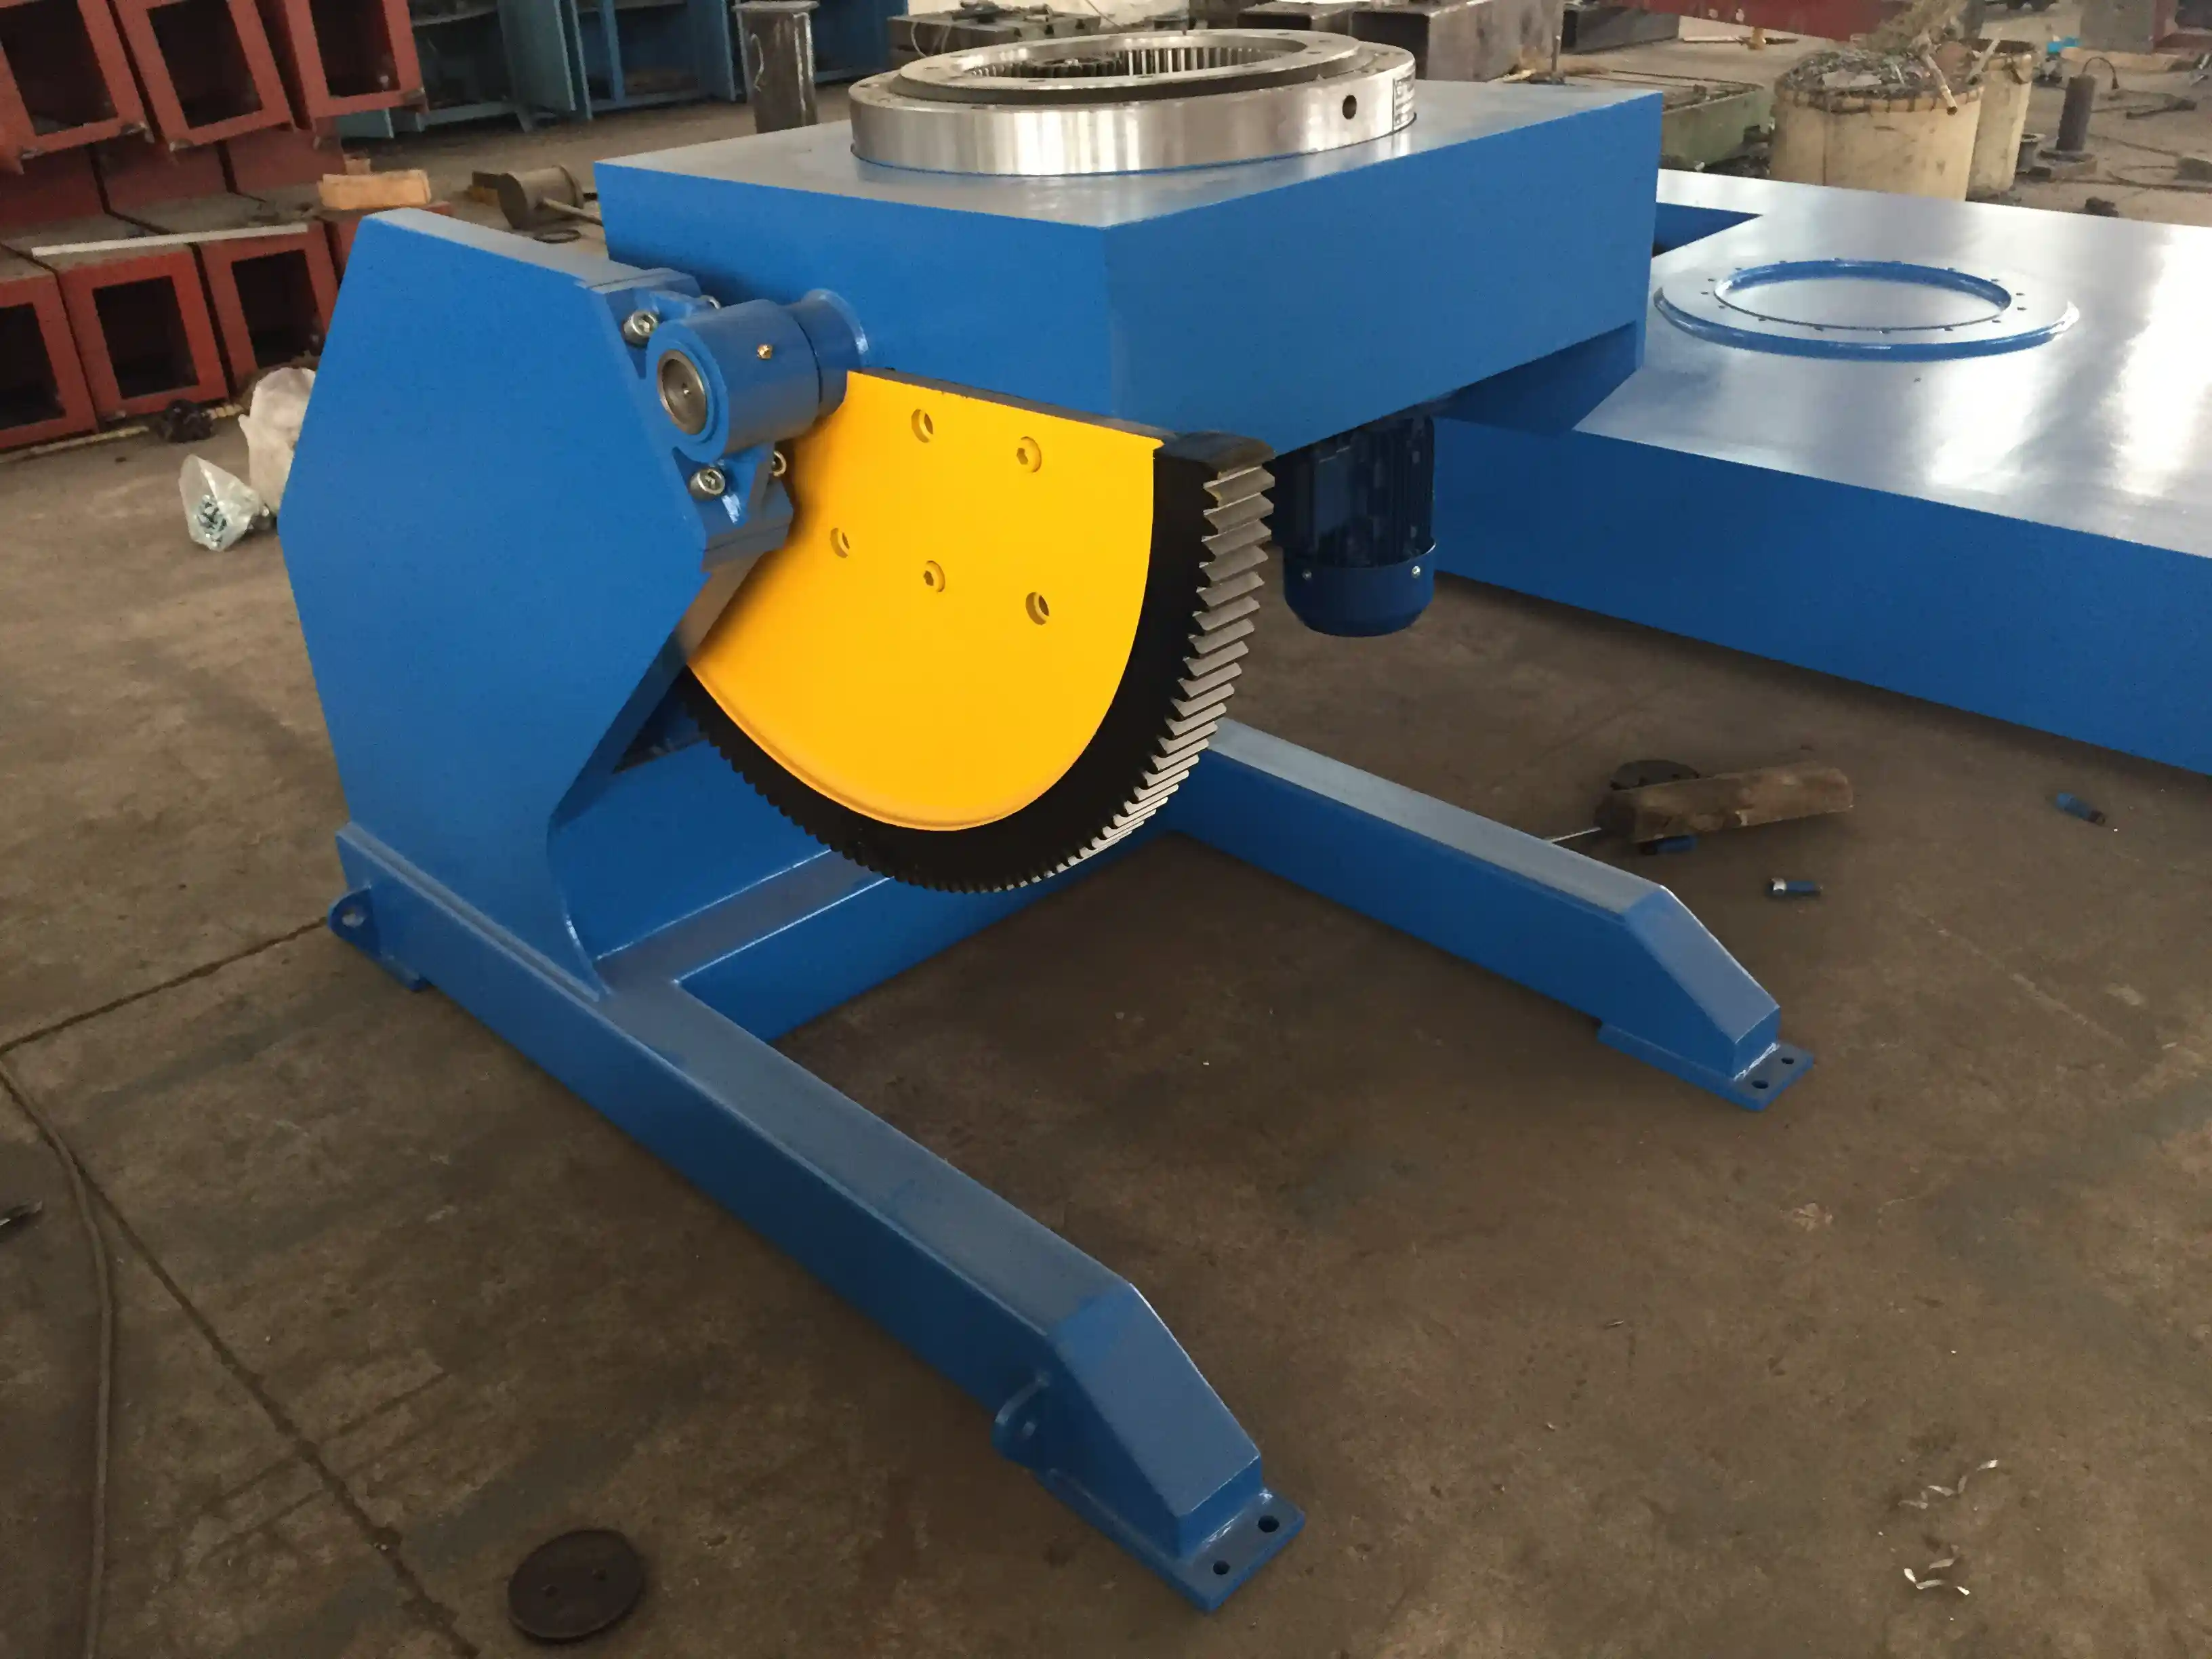
Fixed-height positioners with 1-ton to 5-ton capacity cover many small and medium fabrications. Adjustable-height machines extend that range to 30 tons, 100 tons, or more for large pressure vessels, wind tower sections, and heavy structural weldments. A typical 3-axis table offers 360° continuous rotation, 0° to 90° tilting, and 180° turning, with servo-controlled accuracy in the ±0.05 mm range for robot-ready cells. These specifications matter more than table diameter alone because the load must stay stable through rotation, tilt, and turning.
In tank and pressure vessel fabrication, workpiece rotation is often the fastest way to control welding position and keep circumferential seams consistent. <Melhorar a Qualidade e a Eficiência no Fabrico de Reservatórios e Recipientes sob Pressão: O principal valor de aplicação dos posicionadores> covers how positioners support girth welds and reduce operator handling in cylindrical fabrication.
The positioner also supports robotic welding in ways a fixed table cannot. A servo-driven 3-axis positioner can reorient the workpiece between passes and repeat those orientations program after program. This is critical for automotive, aerospace, and heavy equipment components where weld path accuracy and fixture repeatability determine first-pass yield[2].

Application Comparison: Matching the Job to the Motion
The following table summarizes common fabrication jobs and the preferred primary equipment. In many cases, the final system includes both technologies.
| Application | Preferred primary equipment | Reason |
|---|---|---|
| Long beam and H-beam seams | Manipulador de soldadura | Long linear travel reduces part repositioning |
| Large tank longitudinal seams | Welding manipulator + rotator | Boom covers seam while rotator handles girth |
| Pipe and flange joints | Posicionador de soldadura | Part rotation keeps fillets in position |
| Pressure vessel heads and shells | Welding positioner or manipulator + positioner | Frequent reorientation for nozzle and girth welds |
| Robotic welding cell | Posicionador de soldadura de 3 eixos | Repeatable table orientation for path planning |
| Wind tower sections | Manipulator + positioner/rotator | Long vertical/horizontal seams plus heavy rotation |
| Excavator arms and structural castings | Posicionador de soldadura | Complex multi-pass welds need tilt and turn |
The most productive cells often combine an LH-series manipulator with a 3-axis positioner or adjustable-height turning rolls. The manipulator covers the long seam, while the positioner presents the workpiece for girth, flange, and fillet welds. Matching boom reach, table load, and rotation speed in the same cell reduces setup time and keeps the torch in position longer.
Get a direct configuration recommendation. For load capacity, boom reach, and rotation speed calculations, send your workpiece diameter, maximum weight, weld length, and material to jay@weldc.com or call +86-13815101750. Describe whether the part moves or the torch moves in your current process; a quick review can prevent overbuying or under-sizing.
When Both Systems Belong in the Same Cell
Heavy fabrication lines rarely choose only one motion axis. A wind tower or pressure vessel shop needs the manipulator for longitudinal seams and the positioner or turning rolls for circumferential seams. In these lines, the manipulator handles the straight weld path while the part rotates slowly under a fixed carriage. This keeps the weld puddle in position and reduces the need for vertical-up or overhead welding for long runs.
Robotic cells follow the same logic. The robot performs path tracking, while the positioner presents the joint in the optimal orientation. A 3-axis positioner with PLC or touchscreen control can store pre-set weld programs and communicate with ABB, KUKA, FANUC, and Yaskawa robots. That combination shortens programming time for multi-pass welds and gives the robot a stable reference point for each pass[2].
When multi-position welding is required on complex workpieces, a 3-axis table provides the repeatable orientation that manual fit-up cannot. <Cansado de desafios complexos na soldadura? Como um posicionador de 3 eixos pode aumentar a produtividade em 70%> covers how synchronized rotation and tilt improve robotic welding productivity.

Selection Factors: Load, Reach, and Process Requirements
Start with the weld joint, not the machine spec sheet. Confirm the material type, thickness, welding process, required weld position, and whether the part can be safely lifted and rotated. Then evaluate these factors:
- For positioners: workpiece mass, center-of-gravity distance, table diameter, rotation speed, tilt range, turning angle, and braking/reversing torque.
- For manipulators: boom horizontal travel, vertical travel, rail distance, carriage speed, torch payload, and column stability.
- For combined cells: synchronization between the rotating table or rolls and the welding head, plus the control interface for robot or PLC integration.
- For safety: emergency stops, overload shutdown, anti-fall protection, and machine guarding. Welding equipment must meet applicable machinery safety and qualified welding procedure requirements[3][4].
One common mistake is to size only the workpiece weight and ignore the center-of-gravity offset. A positioner rated for 5 tons may not safely handle a 4-ton part if the load sits far from the table center. The same logic applies to manipulator reach: vertical and horizontal travel must cover the entire joint, including run-on and run-off tabs.
Common Misconceptions
A manipulator can replace a positioner. In a standard configuration, a manipulator does not rotate the workpiece. It can weld long seams and, when paired with turning rolls, girth seams, but it cannot tilt a complex part for multi-axis access.
A positioner is only for round parts. Positioners handle rectangular fabrications, box sections, castings, and weldments when proper tooling is used. The table or fixture secures the part, while tilt and rotation improve weld access.
All rotators are positioners. A welding rotator typically provides one rotation axis for cylindrical workpieces, while a positioner adds tilt or turning axes. For simple pipe girth welds, a rotator may be enough; for complex components, a 3-axis positioner is more versatile.
Get the Right Welding Configuration for Your Project
At WUXI ABK Machinery Co., Ltd., we manufacture welding manipulators, 3-axis positioners, head-and-tail positioners, adjustable-height positioners, and turning-roll systems for heavy fabrication and CNC cutting applications. If you are comparing manipulator reach against positioner capacity—or planning a combined longitudinal and girth welding cell—contact our engineering team for a configuration review.
Email: jay@weldc.com | Tel: +86-510-83555592 | Mobile: +86-13815101750
Explore the Manipulador de soldadura e 3-Axis Welding Positioner technical pages for model parameters and optional features.
Perguntas mais frequentes
Can a welding manipulator rotate the workpiece?
No. In a standard configuration, a manipulator moves the welding head along the boom and rail system. Workpiece rotation requires a positioner, welding rotator, or turning rolls. A manipulator can work with those devices to weld circumferential seams.
Which is better for pressure vessels: a welding manipulator or a welding positioner?
Most pressure vessel shops use both. Turning rolls or a positioner rotate the shell for girth seams, while a manipulator handles longitudinal courses. If only one machine is being added first, a positioner is often more useful for head-to-shell and nozzle welds; a manipulator is more useful for long straight seams.
Can a 3-axis welding positioner be integrated with a robot?
Yes. Many 3-axis positioners use servo axes and PLC or touchscreen control with interfaces for ABB, KUKA, FANUC, and Yaskawa systems. Their repeatable table orientation supports robotic path planning and multi-pass welding.
What specifications should I compare before choosing?
For manipulators, compare boom horizontal travel, vertical travel, rail distance, travel speed, and torch payload. For positioners, compare load capacity, center-of-gravity distance, table diameter, rotation and tilt range, speed, and repeatability. Also check power supply, control interface, and safety features.
Does a welding rotator serve the same purpose as a positioner?
Not entirely. A rotator typically rotates a cylindrical part around its longitudinal axis. A positioner adds tilting or turning axes so the operator can keep the weld in the flat or horizontal position. For simple pipe girth welds, rotators may be enough; for complex components, a 3-axis positioner gives more control.
References
[1] American Welding Society, AWS D1.1/D1.1M:2020, Structural Welding Code—Steel, Miami, FL, 2020.
[2] International Organization for Standardization, ISO 3834-2:2021, Quality requirements for fusion welding of metallic materials—Part 2: Comprehensive quality requirements, Geneva, 2021.
[3] American Society of Mechanical Engineers, ASME Boiler and Pressure Vessel Code, Section IX: Welding, Brazing, and Fusing Qualifications, New York, 2023.
[4] Occupational Safety and Health Administration, 29 CFR Part 1910, Subpart Q: Welding, Cutting, and Brazing, Washington, DC.
Se estiver interessado, consulte estes artigos relacionados:
Wuxi ABK Professional Welding Rotary Equipment: Precision Welding Solution for Pressure Vessel Manufacturing
Dominar a produção pesada: Como os suportes de rolos trepantes se tornam a pedra angular de uma soldadura eficiente
 English
 Español
 Français
 Deutsch
 Português
 Русский