Welding positioners and welding rotators both keep the weld joint moving while the arc stays in a stable, repeatable position. But they are not interchangeable for every job. A positioner grips or supports the workpiece on a table and provides rotation plus some combination of tilt and turning. A rotator cradles a cylindrical part on two or more rollers and rotates it around its longitudinal axis. The difference comes down to part geometry, seam orientation, load distribution, and how many axes the process actually needs.
What Is a Welding Positioner?
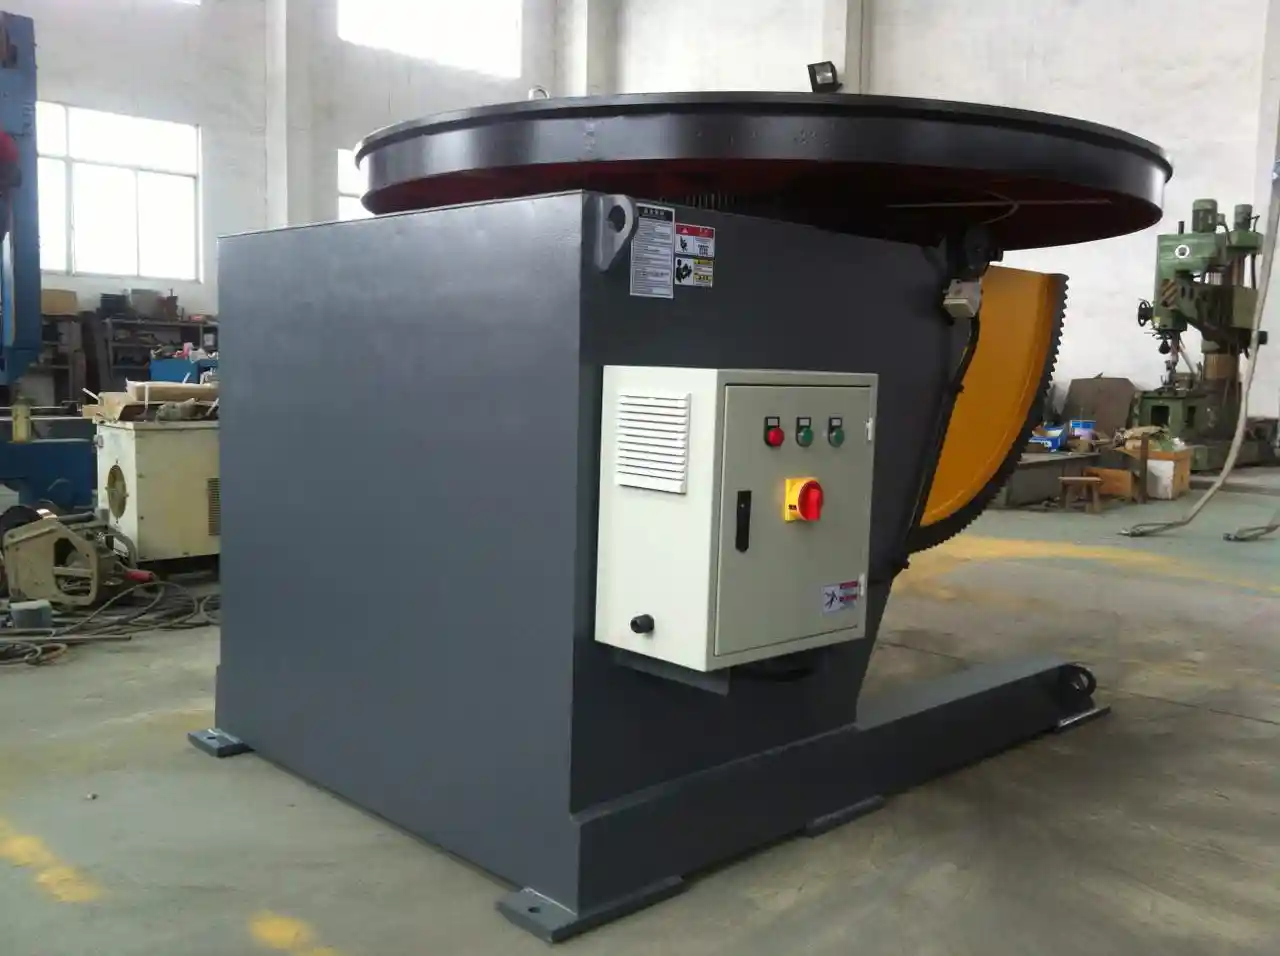
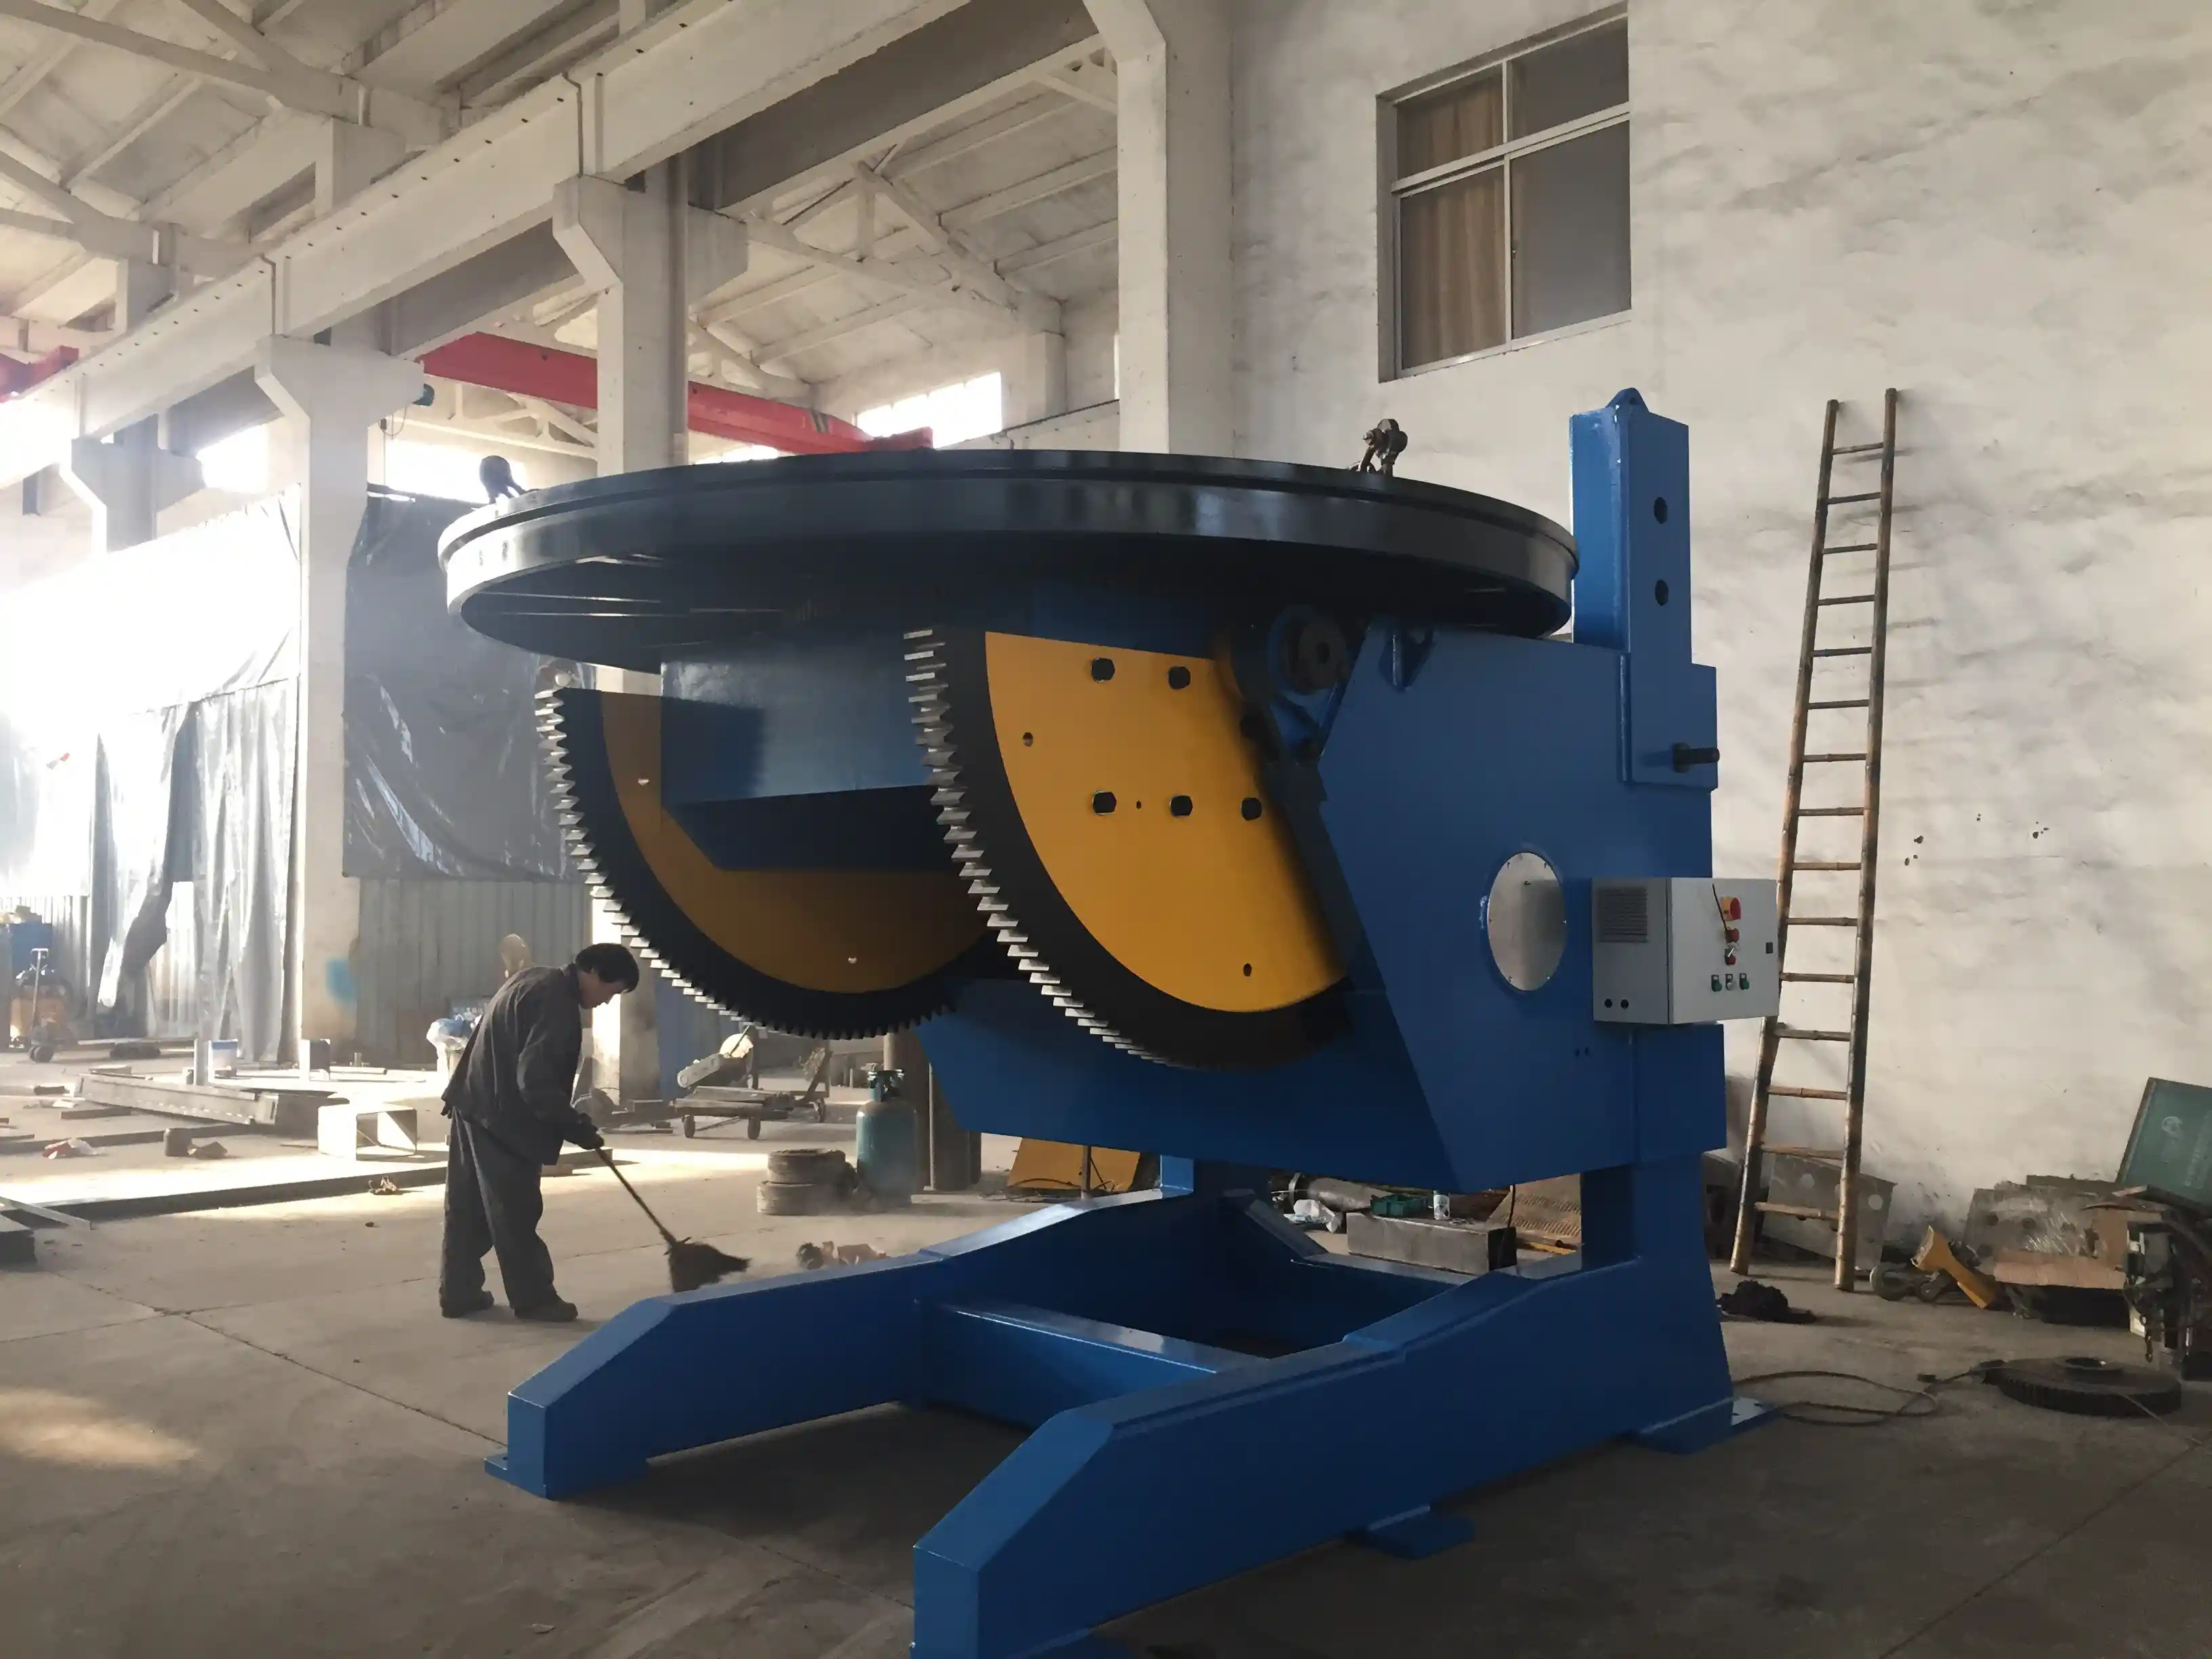
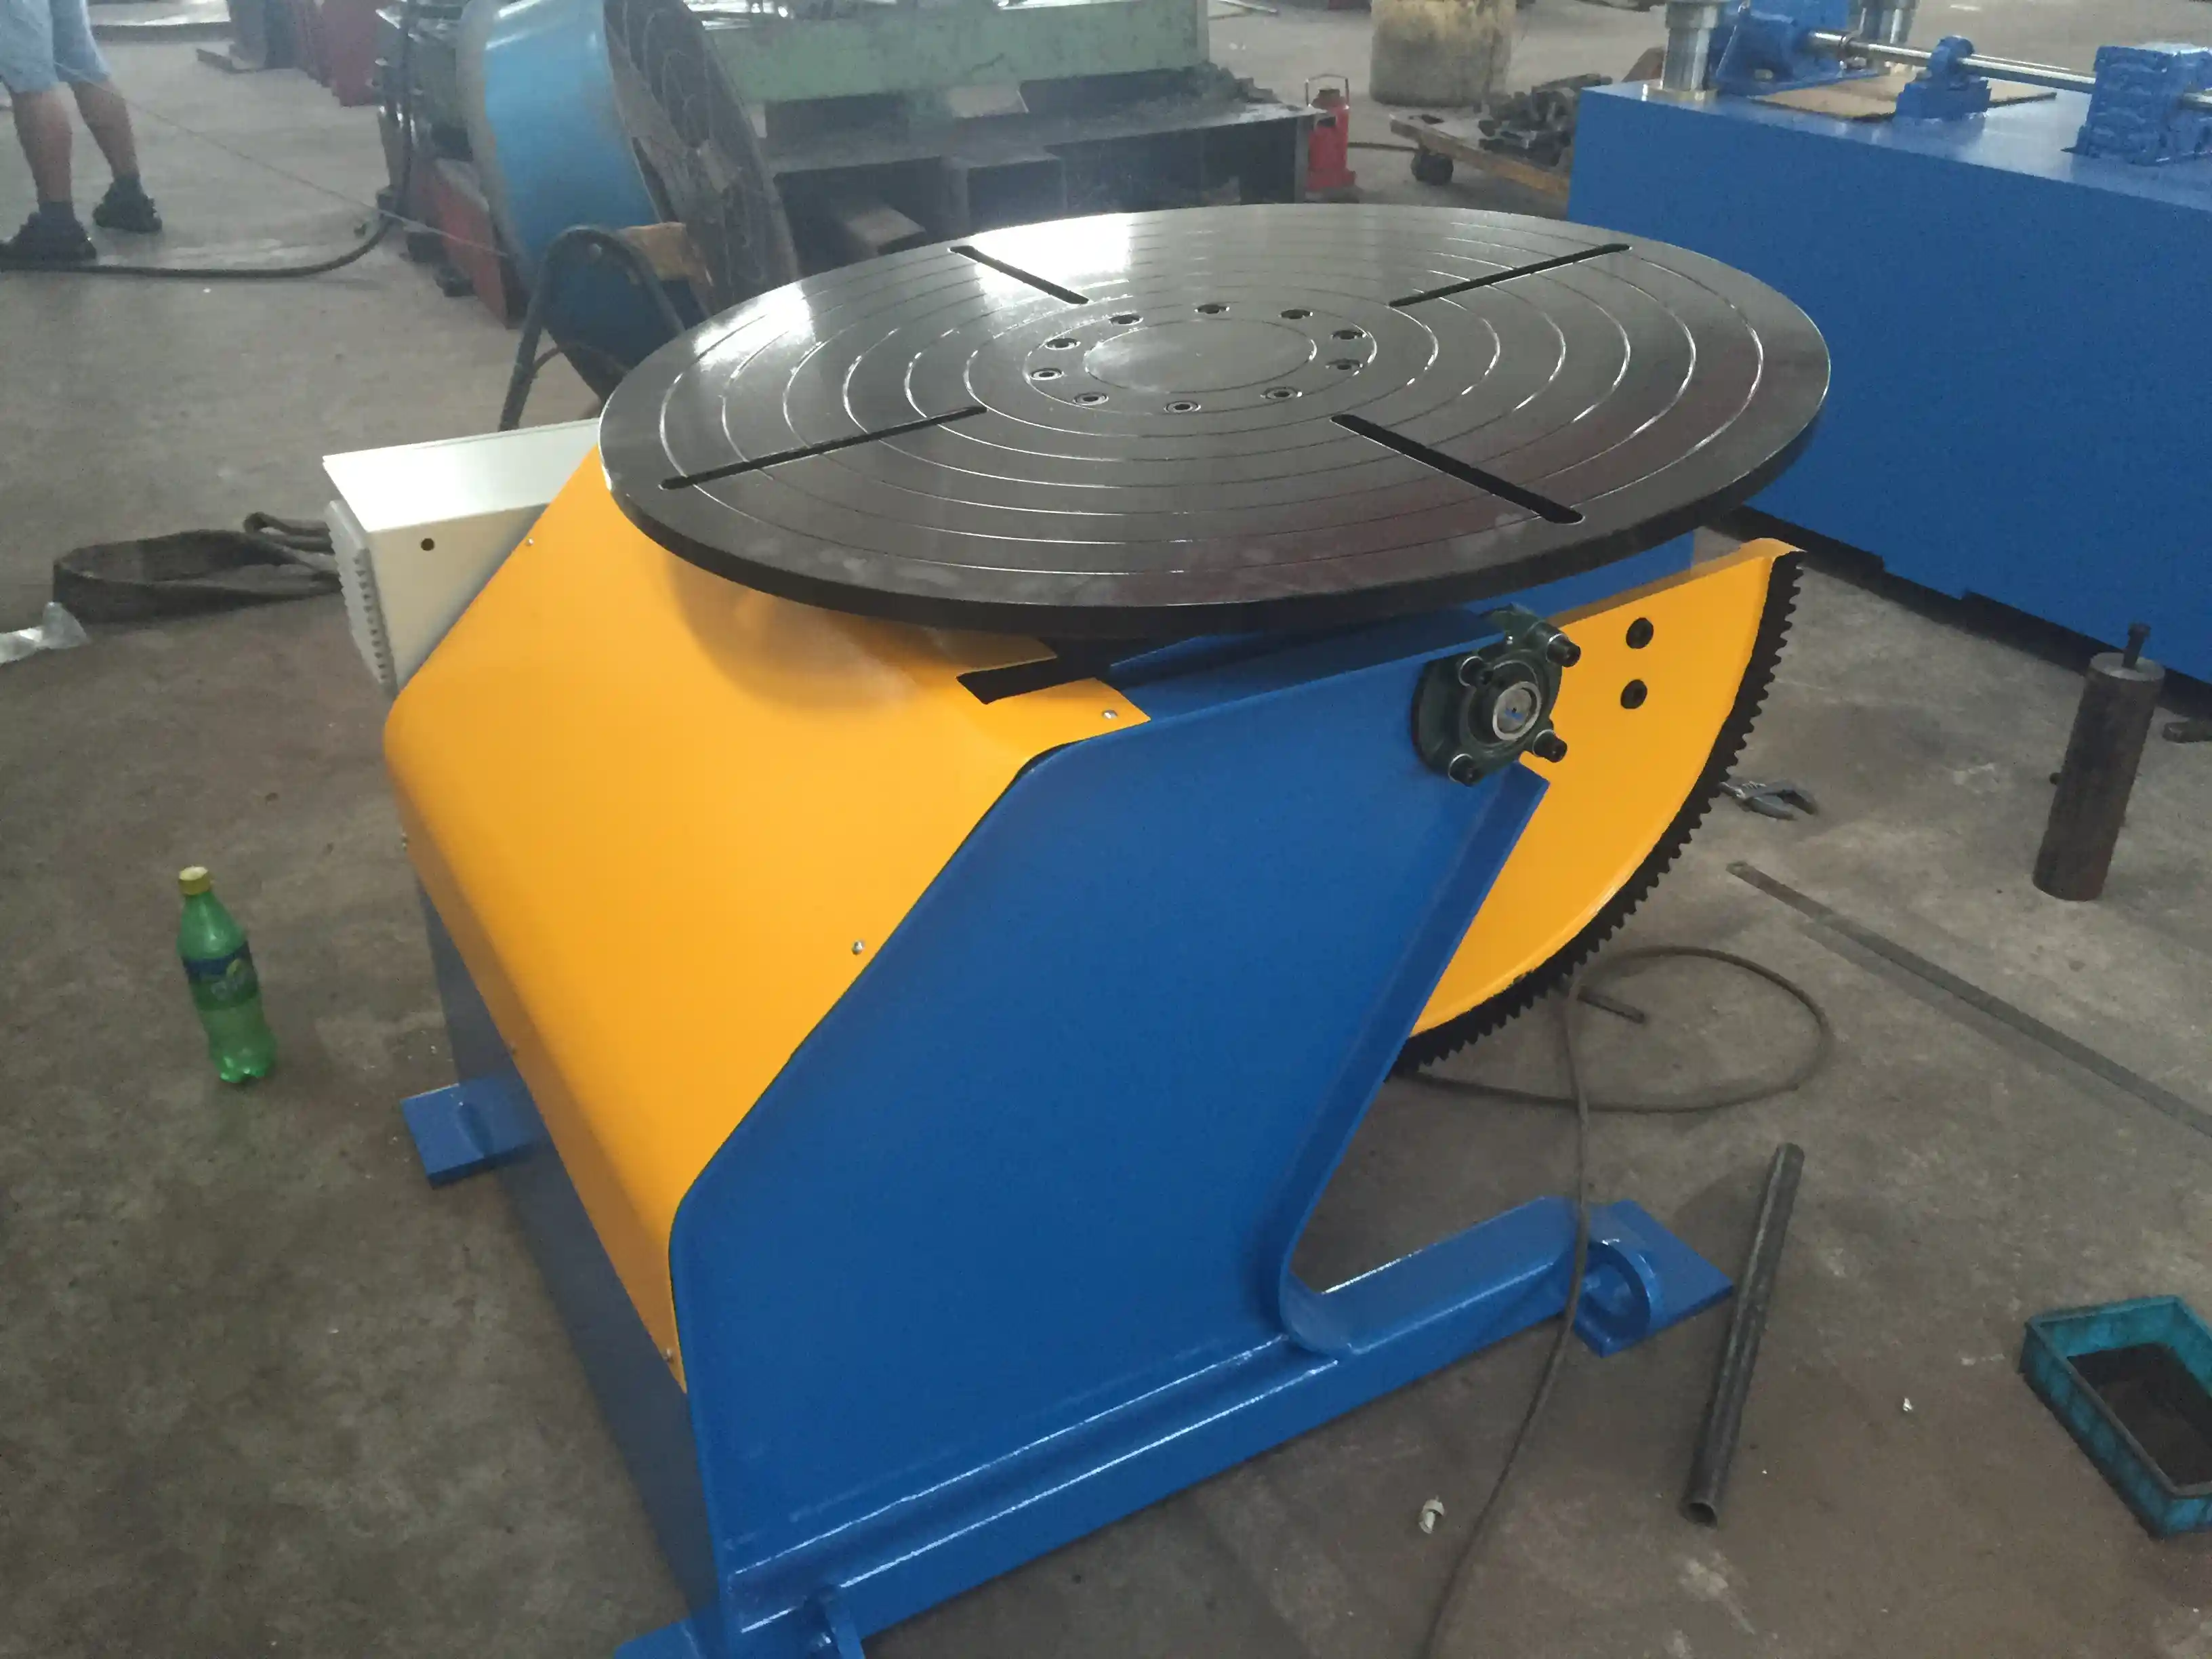
A welding positioner uses a worktable or faceplate to support the component from below. Most models rotate 360° continuously and tilt through a controlled range, commonly 0–135°. In practice, the tilt axis is the main reason fabricators select a positioner: it moves an irregular joint into the flat or horizontal position without unclamping and re-fixturing the part. Higher-level three-axis units add synchronized turning, which further improves access for robotics and multiple-joint components.
ABK positioners cover a broad envelope. Fixed-height units start around 1 ton with a 1200 mm table, while heavier L-type and adjustable-height models reach 30 to 100 tons for pressure-vessel work. The controls are built around PLC and HMI interfaces, with stepless speed regulation and robot compatibility for MIG, TIG, and submerged-arc cells. Structural steel fabricators often use positioners for crane segments, excavator booms, wind-tower flanges, and vessel heads because these parts rarely have a single simple centerline. Under AWS D1.1 structural welding conditions, tilting the workpiece helps operators keep fillets and groove welds within qualified positions [1].
What Is a Welding Rotator?
A welding rotator, often called turning rolls or pipe rotators, supports a cylindrical workpiece on driven and idler roller frames. The rollers contact the outside diameter and rotate the shell so a welding head, manipulator, or operator can remain in one downhand position. Rotators are specialized for continuous girth welding—not for repositioning irregular parts.
The selection starts with vessel diameter and total weight. ABK standard and adjustable rotators cover approximately 5 to 300 tons, with diameter ranges from roughly 250 mm on small models to 6000 mm on heavy-duty systems. Drive speed is usually adjustable, either 100–1000 mm/min or 0.5–5 RPM depending on the frame, and anti-creep controls limit axial drift during long welds. For long pipes, storage tanks, wind-tower sections, and pressure-vessel shells, the rotator is frequently the most cost-effective option because it replaces manual chain fall turning or crane-assisted repositioning.
Positioner vs Rotator: Core Differences at a Glance
| Fator | Posicionador de soldadura | Rotador de soldadura |
|---|---|---|
| Workpiece support | Table or faceplate under the part | Roller frames under the outside diameter |
| Primary motive axes | Rotation + tilt; 3-axis adds turning | Single rotational axis, driven rollers |
| Part geometry | Irregular, flanged, structural, box, heavy castings | Cylindrical shells, pipes, tanks, vessels |
| Load control | Table capacity and eccentric/center-of-gravity limits | Roller load distribution and anti-creep control |
| Typical application | Downhand repositioning of complex joints | Continuous circumferential or girth welding |
| Integration | PLC/HMI, robot interface, ±0.5° or tighter on high-precision models | Frequency conversion speed control, manipulador de soldadura interface |
The table shows the central decision: choose a positioner when the part would otherwise need repeated manual turning; choose a rotator when the workpiece is already cylindrical and the main need is slow, stable rotation.
Quick Decision Help
If you are comparing both machine types for an active project, send the workpiece drawing, weight, and weld seam list to jay@weldc.com. Include the maximum diameter or table footprint, required tilt, and whether the welding will be manual, column-and-boom, or robotic. This one inquiry usually returns a direct equipment recommendation and a suggested process layout.
When a Welding Positioner Wins
A positioner wins when the component is not a simple cylinder or when the weld joint must change orientation several times within the same sequence. Structural frames, boom segments, pump housings, flanged pipe assemblies, vessel heads, and wind-turbine flanges often have multiple groove and fillet seams that are difficult to weld in a single flat position.
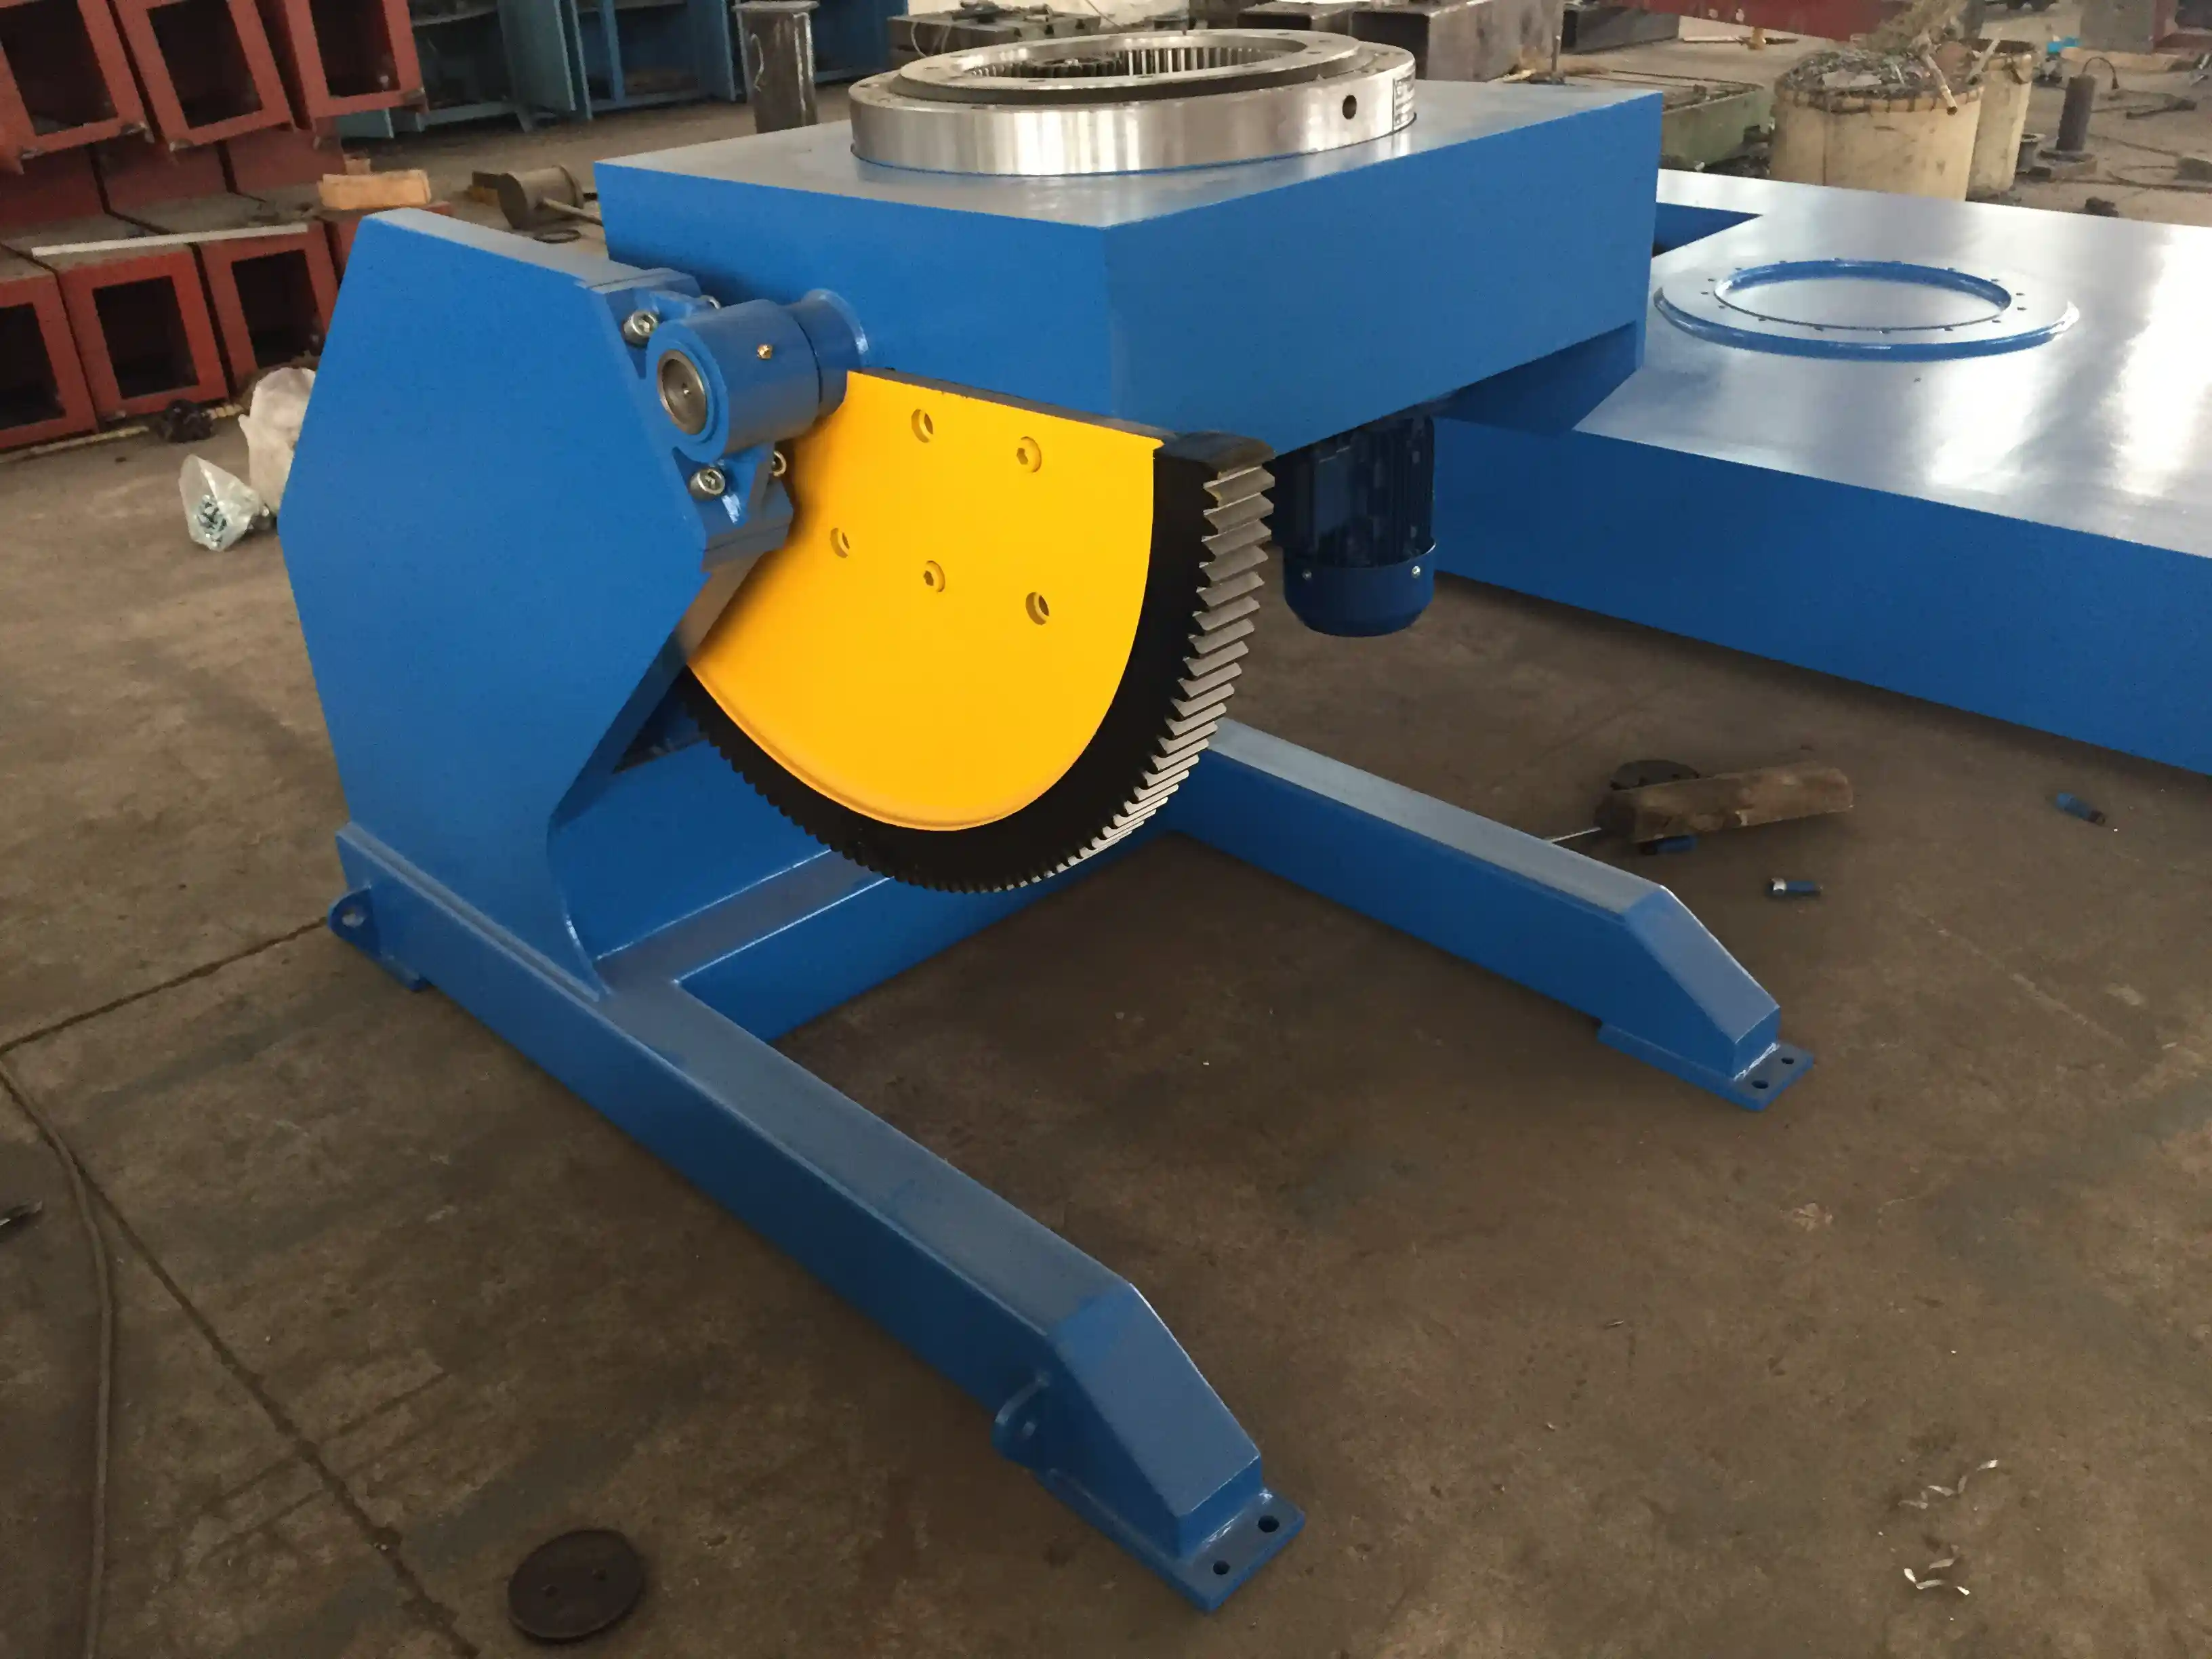
Here, rotation alone is not enough. The table supports the part while the tilt axis brings each joint into a comfortable, repeatable welding angle. That reduces weld metal overflow, undercut risk, and operator fatigue in manual or semi-automatic cells. In robotic cells, the positioner acts as the coordinated external axis so the torch can maintain the same orientation while the part moves.
Non-axisymmetric parts require more than rotation. <Tired of Complex Welding Challenges? How a 3-Axis Positioner Can Boost Productivity by 70> covers how ABK positioners handle complex weld angles and part changes.
When a Welding Rotator Wins
A rotator wins when the workpiece is naturally supported on rollers and the main task is circumferential welding. Pipe spools, tank courses, pressure-vessel shells, wind-tower cans, and cylindrical heat-exchanger bodies all fit this profile. The drive rollers rotate the part at a constant surface speed, while the welding manipulator or operator stays in one position.
In these applications, a rotator reduces setup time and keeps long girth welds uniform. Because the rollers distribute load over line contacts, the design must match wheel spacing and diameter to the shell; otherwise, thin-wall vessels can deform or drift. Anti-creep systems and idler frame adjustment help maintain joint position over long welds.
For long cylindrical shells, a rotator provides stable continuous rotation while the welding head stays in one downhand position. <Rotadores de tubos e rolos de torneamento: Equipamento essencial para o fabrico moderno de condutas> covers how ABK roller systems handle drive and idler frame selection for different diameters.
How to Decide: Load, Geometry, Axis Requirements
Start with the seam map and the workpiece centerline. If the part can roll on its outside diameter and most of the welding is circumferential, a rotator is the natural choice. If the part has flanges, reinforcing pads, nozzles, brackets, or changes in cross-section—and if the seam orientation changes—a positioner is the better starting point.
Use this sequence:
- List every weld joint and its required position.
- Measure maximum weight, diameter or width, and center-of-gravity offset.
- Decide whether the process needs rotation only or rotation plus tilt.
- Check robot or manipulator interface requirements.
- Confirm whether the part can tolerate roller contact or must be table-supported.
For shops working under ISO 3834-2 welding quality requirements, equipment selection is also part of welding coordination and should be reviewed before the process is finalized [2]. When the role of the welding coordinator includes equipment adequacy, the choice between positioner and rotator affects joint accessibility, repeatability, and process documentation [3].
Tank and pressure-vessel fabricators frequently use both machines on the same production line. A rotator handles the long shell courses, while a positioner handles heads, nozzles, flanges, and complex subassemblies. This combined approach often reduces re-fixturing and balances the skill load across the shop.
Tank and pressure-vessel fabricators often use both: positioners for heads/nozzles and rotators for shell girth seams. <Melhorar a Qualidade e a Eficiência no Fabrico de Reservatórios e Recipientes sob Pressão: O principal valor de aplicação dos posicionadores> covers how ABK positioners reduce rework on vessel heads, nozzle welds, and off-axis joints.
Talk to a Welding Automation Engineer
Need a positioner or rotator recommendation for your next project? Send the following to jay@weldc.com:
- Workpiece drawings or main dimensions
- Maximum weight and center-of-gravity offset
- Welding process and automation or robot requirements
- Seam types and target output per shift
Wuxi ABK Machinery will reply with a technical recommendation, proposed layout, and capacity range based on the load and geometry you supply.
Perguntas mais frequentes
Is a welding rotator the same as a welding positioner?
No. A rotator supports a cylindrical part on rollers and provides one rotational axis. A positioner supports the part on a table and typically adds tilt, with some models adding a third turning axis.
Can a welding positioner rotate a cylindrical tank shell?
Yes, but for very long shells a rotator is usually more efficient. A positioner works better for vessel heads, nozzles, flanges, and other non-cylindrical details, while a rotator handles the long straight-shell girth seams.
What information does the supplier need before selecting?
Share the workpiece dimensions and weight, center-of-gravity offset, weld types, required tilt, automation interface, and production target. This lets the supplier confirm capacity, rotation speed, and control requirements.
Can both machines integrate with robotic welding?
Yes. Positioners often operate as coordinated robot axes, and rotators can interface with welding manipulators or robot control systems through PLC communication and encoder feedback.
Does a positioner require more maintenance than a rotator?
Both need daily cleaning and lubrication checks. A positioner has more axes, tilt gearing, and possibly slip rings, so the scheduled inspection scope is larger. A rotator requires less daily intervention but still needs roller wear and anti-creep checks.
References
[1] AWS D1.1/D1.1M:2020, Structural Welding Code—Steel.
[2] ISO 3834-2:2021, Quality requirements for fusion welding of metallic materials — Part 2: Comprehensive quality requirements.
[3] ISO 14731:2019, Welding coordination — Tasks and responsibilities.
Se estiver interessado, consulte estes artigos relacionados:
Principais pontos problemáticos e soluções de alta precisão dos posicionadores de soldadura nas indústrias da energia eólica e da construção naval: Análise técnica exaustiva
Dominar a produção pesada: Como os suportes de rolos trepantes se tornam a pedra angular de uma soldadura eficiente
Baixa eficiência na soldadura em grupo de tubagens: como os suportes de rolos inteligentes aumentam a produtividade em 50%
Solução revolucionária para a soldadura de vasos de pressão: Análise técnica de posicionadores de soldadura rotativos de 360 graus
Desafios da soldadura em torres eólicas: como os sistemas hidráulicos de elevação avançados aumentam a produção em 40%
 English
 Español
 Français
 Deutsch
 Português
 Русский