
Welding positioner factories sit between steel fabrication, machine building, and welding process control. A well-built positioner does more than rotate a workpiece. It stabilizes the joint position, controls travel speed, and reduces the physical strain and inconsistency that come with manual out-of-position welding. For fabricators purchasing heavy equipment, the central question is not only how many tons the machine can carry, but how the factory manages design, machining, assembly, and final verification before the unit reaches the shop floor.
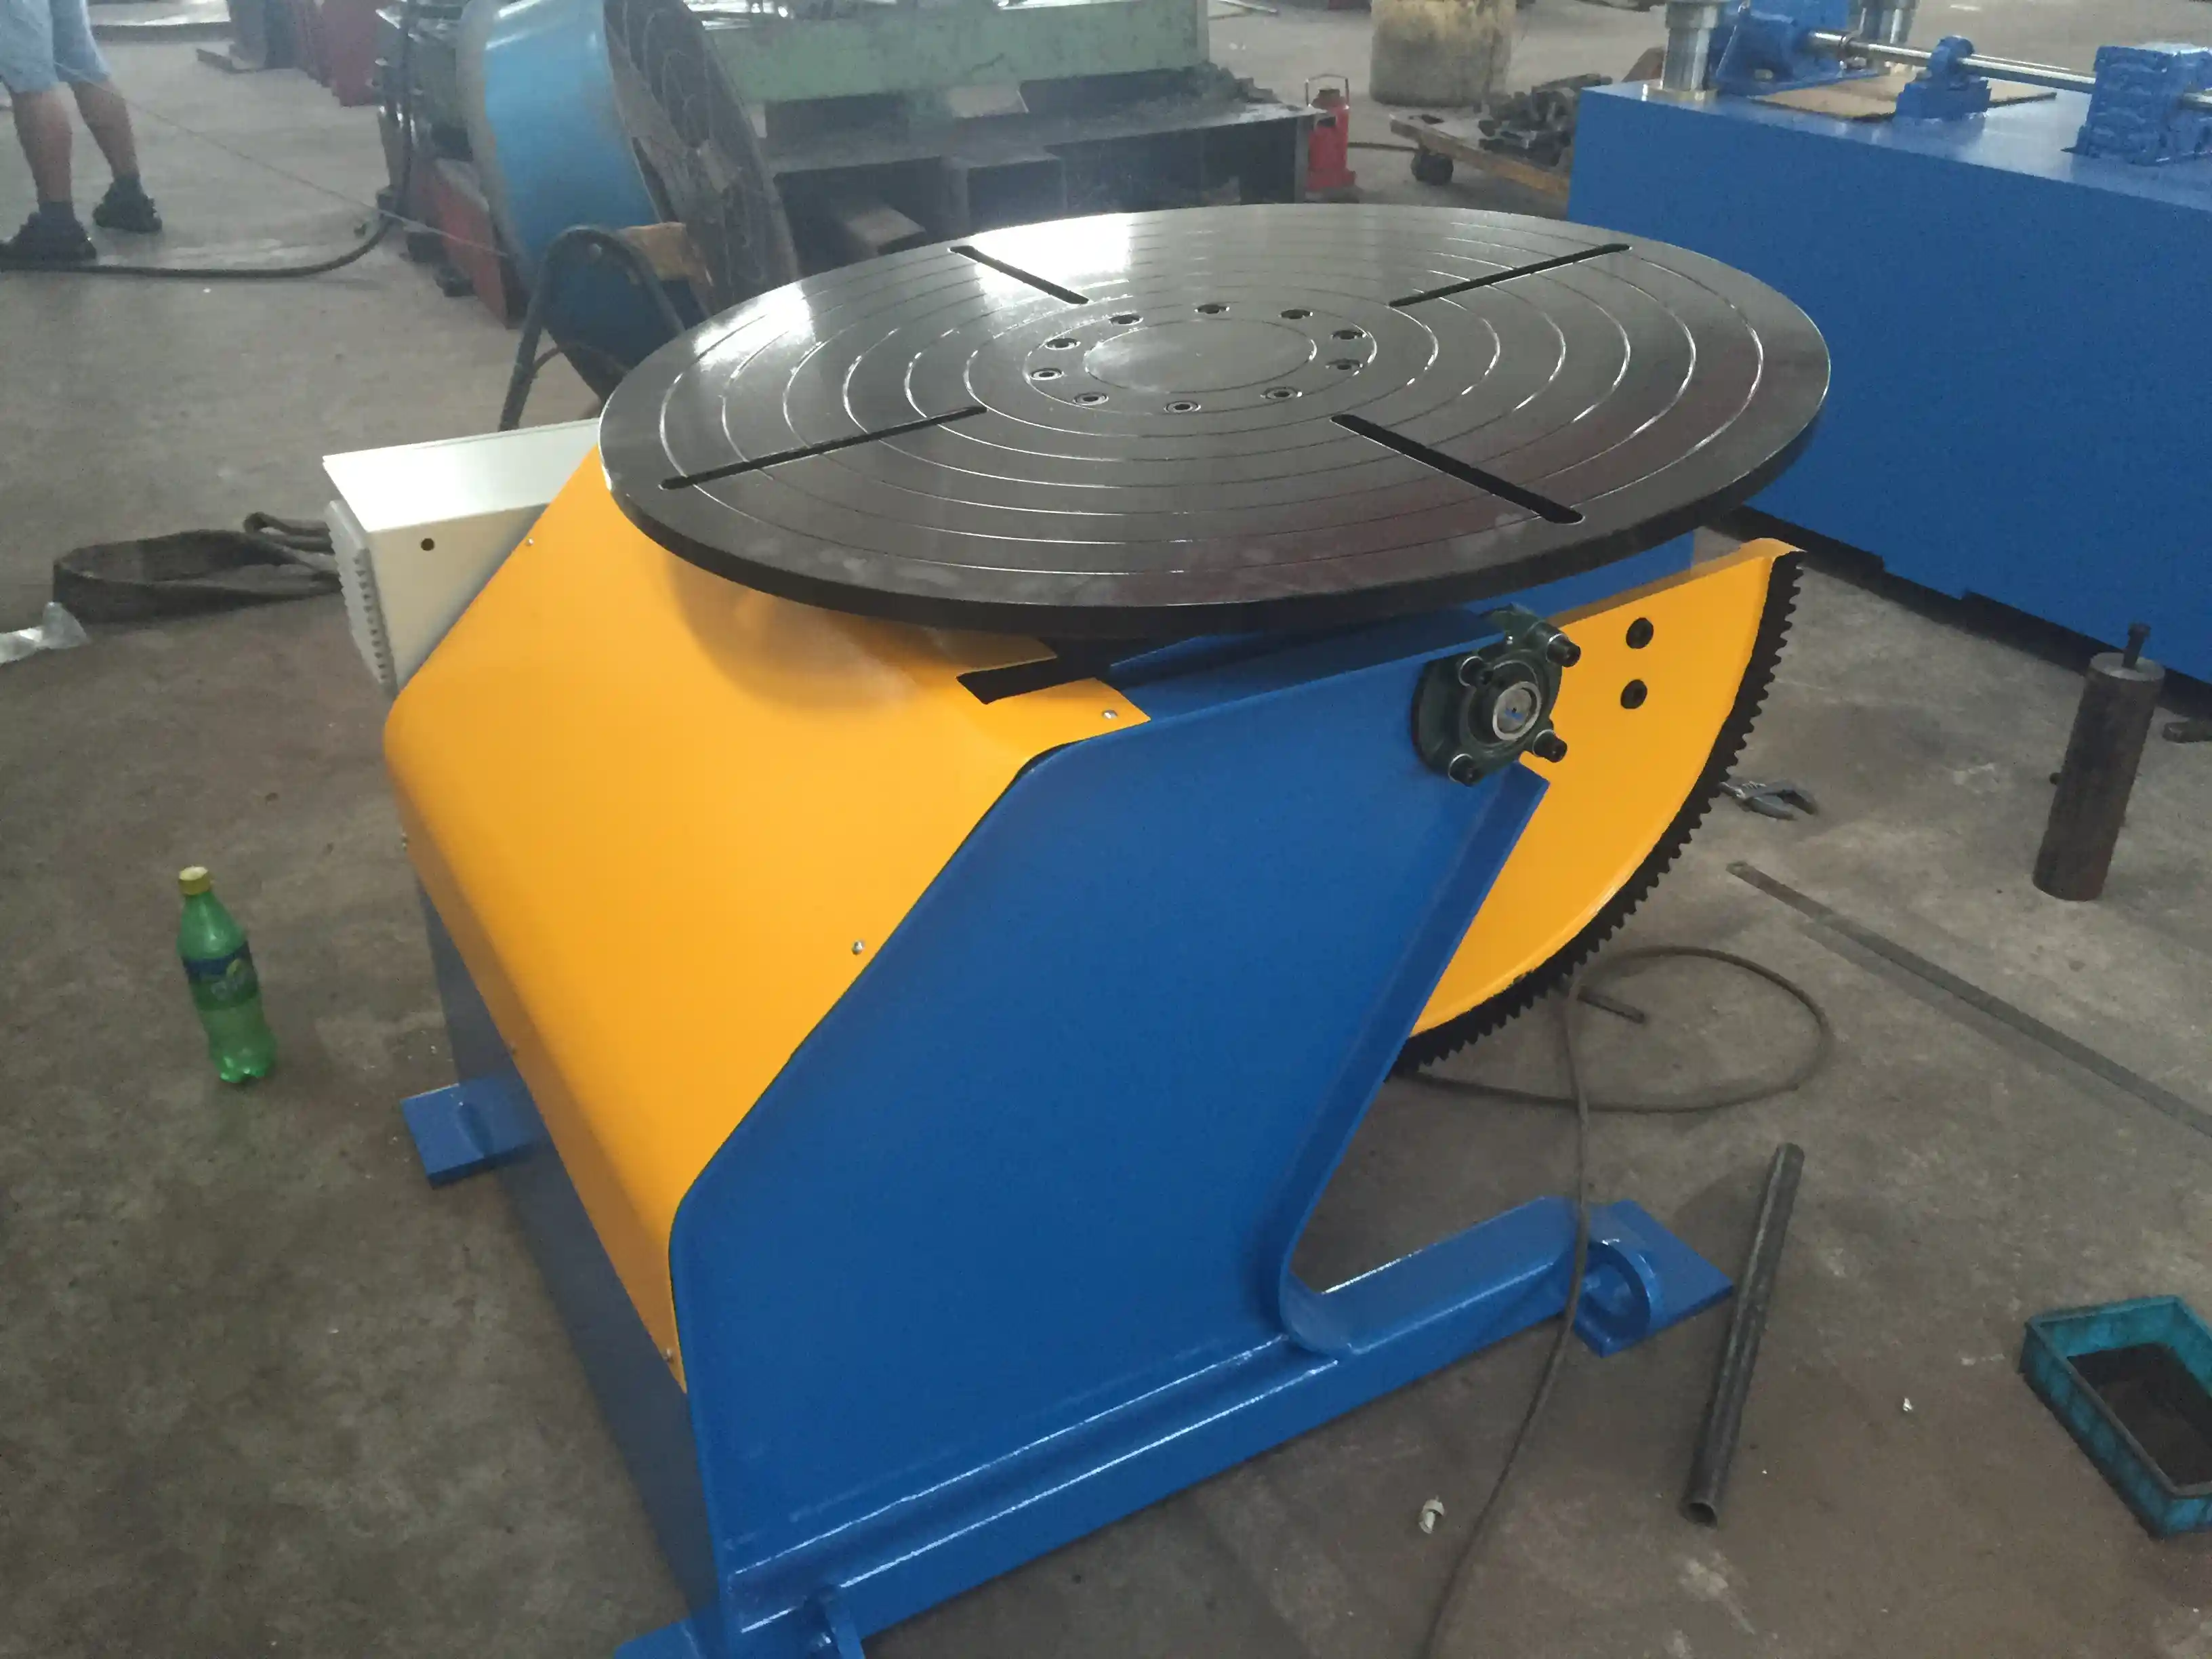
How Welding Positioner Factories Influence Weld Quality
Positioner quality directly affects weld process control. If the table rotates unevenly, the torch angle and travel speed change during the pass. If the tilt axis drifts under load, the weld puddle shifts. These small deviations accumulate over a long seam and become missed fusion, undercut, or rework.
A welding positioner factory therefore needs to control three related characteristics: rotational stability, positioning repeatability, and load-bearing behavior under eccentric or offset center-of-gravity conditions. That is not only a mechanical concern. For fabricators working to ISO 3834-2, welding coordination includes controlling equipment used during production, not just the weld procedure [1]. A positioner is part of that controlled production system.
The base frame, table, reducer, motor, and control system all need to be selected as a matched system. A factory that treats the positioner as a simple rotary fixture may deliver a unit that rotates on an empty table but no longer holds tolerance under real workpiece load.
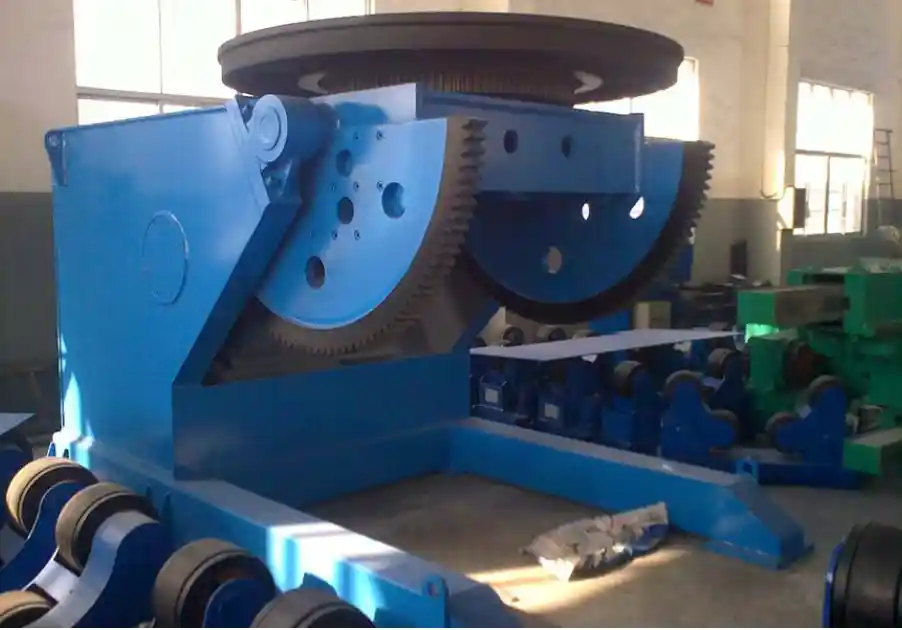
In practice, positioner accuracy is validated through the welding result, not only the machine catalogue data. <Comment améliorer la qualité du soudage de tubes grâce à un positionneur de soudage de haute précision> covers the relationship between positioning accuracy, travel control, and repeatable pipe weld quality.
Core Engineering Checks for High-Quality Production Equipment
When comparing positioner factories, focus on engineering decisions that affect long-term performance.
- Frame and base construction: The base should be stress-relieved and rigid enough to resist deformation under dynamic load. A heavy casting or box-type steel structure is expected for medium and heavy positioners.
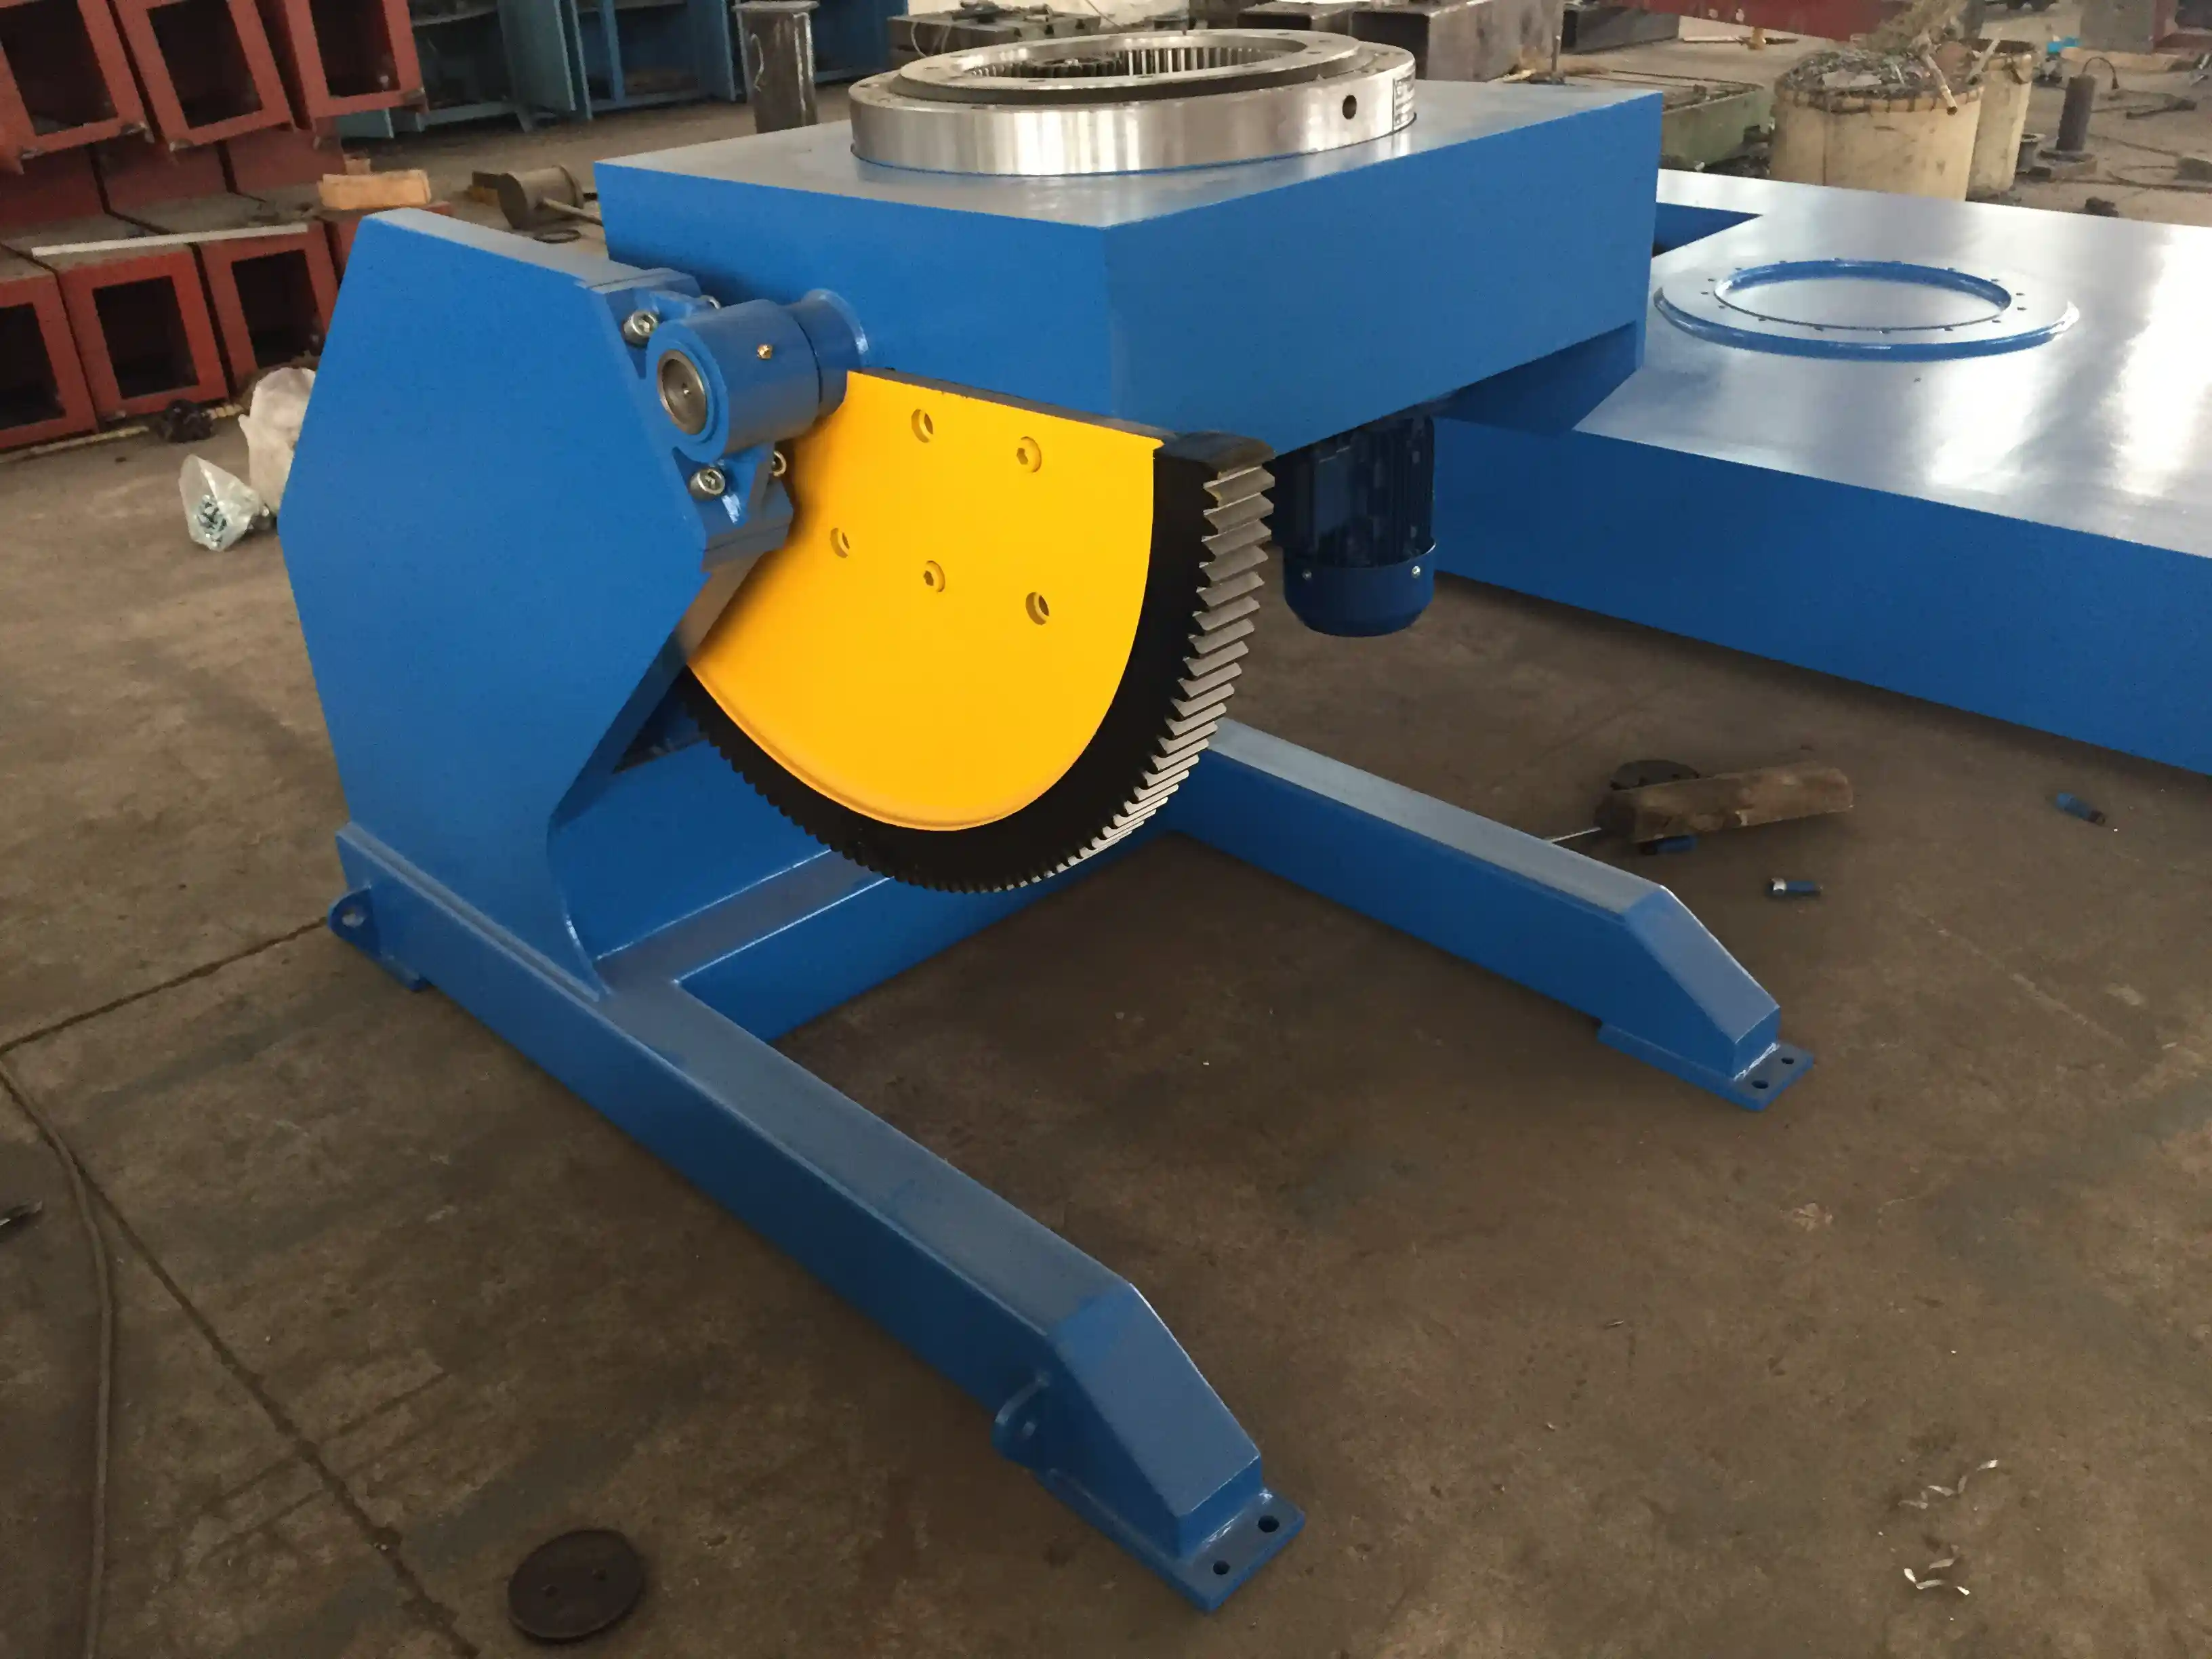
- Slewing bearing and reducer: These components determine backlash, smoothness, and torque delivery. High-quality factories specify bearings and reducers that can support axial, radial, and overturning loads at the same time.
- Drive and braking: Rotation and tilt should be stepless or servo-controlled. Braking must hold the table when power is interrupted, especially for tilted loads.
- Control integration: PLC or HMI control should allow preset weld programs, jog operation, and robot interface where required.
- Safety systems: Emergency stop, overload protection, and anti-fall devices need to be verified as part of factory acceptance.
Under a quality management system such as ISO 9001, a positioner factory must control purchased materials, machining, assembly, and final verification, not only final inspection [2].
Representative fixed and adjustable configurations used in heavy fabrication are shown below.
| Configuration | Load capacity | Table diameter | Rotation speed | Précision du positionnement | Typical application |
|---|---|---|---|---|---|
| 1-ton fixed-height | 1,000 kg | 1,200 mm | 0.05–0.5 RPM | ±0,5° | Flanges, small structural parts, general fabrication |
| 5-ton fixed-height | 5,000 kg | 1,500 mm | 0.05–0.5 RPM | ±0,5° | Pressure vessels, rail bogie assembly, structural steel |
| 5-ton adjustable-height L-type | 5,000 kg | 900 mm | 0.05–0.5 RPM | ±0,5° | Pipe fabrication, wind tower components, robotic cells |
| 30-ton adjustable-height | 30,000 kg | 600 mm L-support | 0.05–0.5 RPM | ±0,5° | Heavy structural steel, pressure vessels, large-position welding |
| 100-ton adjustable-height | 100,000 kg | 1,800 mm | 0.05–0.5 RPM | ±0,5° | Wind tower sections, heavy cylindrical structures |

Matching Positioner Configuration to the Fabrication Task
The correct positioner configuration depends on workpiece geometry, weld position, and production volume.
Fixed-height positioners suit shops that process similar part families and do not need frequent table height changes. Adjustable-height and L-type positioners help when the weld seam must be brought to a comfortable working height or when long components require support at both ends.
For structural applications, the positioner must support the joint orientations and tolerances required by the applicable welding code, such as AWS D1.1 [4]. A positioner that cannot hold the specified root opening or maintain alignment during welding will create nonconformities before the welder makes a single pass.

For wind tower and shipbuilding work, the challenge is combining heavy sections with long seam access. <Principaux problèmes et solutions de haute précision des positionneurs de soudage dans les secteurs de l'énergie éolienne et de la construction navale : Analyse technique complète> covers how positioner design supports large-diameter and high-precision fabrication.
Pressure vessel fabrication adds code-driven joint access requirements that influence positioner selection. <Solution révolutionnaire pour le soudage des appareils à pression : Analyse technique des positionneurs de soudage rotatifs à 360 degrés> covers 360-degree rotating positioner configurations for circumferential and longitudinal seams.
Factory Production, Inspection, and Compliance
A serious welding positioner factory should be able to demonstrate its production and inspection sequence, not just a finished catalogue. Key checks include material traceability, machining tolerances, drive calibration, load testing, and electrical safety verification.
CE-marked positioners must satisfy the essential health and safety requirements of the Machinery Directive [3]. A factory that exports into regulated markets should provide the relevant declaration and technical file evidence. In addition, many buyers require ISO 9001 quality management certification as a minimum factory-level control [2].
For welding equipment that affects weld quality, ISO 3834 provides a useful framework for welding-related quality requirements [1]. Even when the buyer does not require full ISO 3834 certification, the same logic applies: welding equipment should be capable of maintaining the process conditions specified in the welding procedure.
Evaluating a Welding Positioner Factory Before Purchase
Before placing an order, buyers should request more than a price. Ask for the following:
- Machining and assembly records for critical components
- Load test or run-in procedure used before shipment
- Control system documentation and electrical drawings
- Available robot interface signals and communication protocols
- CE marking and applicable compliance documents
- Warranty coverage and spare parts availability
A factory visit or video inspection can reveal how the manufacturer handles raw material storage, welding, stress relief, machining, painting, and final assembly. The goal is to confirm that the production process supports repeatable machine quality.
Engineering support check: If you are matching a new positioner to a specific weld procedure, send the maximum workpiece weight, center-of-gravity offset, required rotation speed, and available power supply to jay@weldc.com. A direct technical review will clarify whether you need a fixed, adjustable-height, or 3-axis configuration.
Request a Configuration Review and Quotation
WUXI ABK MACHINERY CO., LTD has manufactured welding equipment and CNC cutting machines since 1999. The company supplies welding positioners, manipulateur de soudages, rotators, H-beam welding lines, soudage des mâts d'éolienne lines, and complete fabrication systems for demanding heavy-industry applications.
To request a configuration review, provide the following information in your inquiry list:
- Workpiece type and welded joint description
- Maximum workpiece weight and dimensions
- Center-of-gravity distance or offset
- Required rotation and tilt angles
- Welding process and automation level
- Factory voltage and frequency
Send the technical details to jay@weldc.com or contact the team at +86-13815101750. The engineering team will recommend the smallest positioner that supports the required accuracy, clearance, and load behavior without oversizing the machine.
Questions fréquemment posées
What does a welding positioner factory actually control for weld quality?
The factory controls frame rigidity, bearing and reducer selection, drive response, table flatness, tilt accuracy, and safety systems. These characteristics determine whether the positioner maintains the weld joint in a stable position during rotation and tilting.
How do I choose between a fixed-height and adjustable-height welding positioner?
Choose fixed-height when part sizes are consistent and the weld seam height does not change often. Choose adjustable-height or L-type configurations when the shop welds different diameters, long sections, or parts that require height adjustment for operator and torch access.
What load capacity should I specify?
Specify capacity based on the maximum workpiece weight plus fixture weight. Also account for eccentric loads. If the center of gravity is not centered on the table, the effective overturning moment may require a higher capacity or additional support.
How are positioning accuracy and repeatability verified?
The factory should provide measured test data from a load test or run-in procedure. Buyers should ask how table runout, backlash, and tilt repeatability are checked before shipment and whether robot interface tests are performed for automated cells.
What information should I send to a positioner factory for a quotation?
Send the workpiece weight, dimensions, center-of-gravity offset, required rotation and tilt angles, welding process, automation level, and power supply. This information allows the factory to recommend a configuration based on load behavior, not only table capacity.
References
[1] ISO 3834-2:2021, Quality requirements for fusion welding of metallic materials — Part 2: Comprehensive quality requirements, International Organization for Standardization.
[2] ISO 9001:2015, Quality management systems — Requirements, International Organization for Standardization.
[3] Directive 2006/42/EC of the European Parliament and of the Council of 17 May 2006 on machinery, Official Journal of the European Union.
[4] AWS D1.1/D1.1M:2020, Structural Welding Code — Steel, American Welding Society.
Si cela vous intéresse, consultez ces articles connexes :
Une révolution dans le domaine du soudage naval : comment les positionneurs de soudage améliorent la qualité et l'efficacité
Manipulateurs de soudage pour la fabrication de tours éoliennes : Révolutionner l'efficacité de la production
Améliorer la qualité et l'efficacité dans la fabrication de l'énergie éolienne : Le rôle clé des positionneurs dans le soudage des sections de tours
Une valeur ajoutée exceptionnelle : comment les positionneurs de soudage à hauteur fixe favorisent les avancées dans les secteurs de la construction navale et offshore (2e partie)
 English
 Español
 Français
 Deutsch
 Português
 Русский